
Standard & Custom Polyamide Semi-Finished Stock
Premium factory-direct extruded and cast engineering plastic rods, tubes, and sheets ready for prompt international dispatch.






The Global Polyamide (PA) Landscape: Modern Industrial Evolution
Strategic shift toward lightweight, corrosion-proof, and self-lubricating engineering polymers in heavy machinery, automotive assembly, and renewable equipment.
Metal-to-Plastic Conversion Trends
Global Tier-1 manufacturers are replacing phosphor bronze, cast iron, and aluminum alloys with high-crystallinity cast nylon (PA6G) and extruded PA66. Polyamide offers an 85% mass reduction over bronze, dramatically lessening rotational inertia, lowering system energy consumption, and eradicating galvanic corrosion in maritime or chemical environments.
Tribological Performance
Modern automated machinery demands unlubricated run-dry resilience. By compounding primary caprolactam monomer with liquid lubricant dispersions (Oil-Filled Nylon) or micro-particulate MoS2 (Molybdenum Disulfide), dynamic dry friction coefficients drop from 0.38 down to 0.12, terminating stick-slip phenomena and reducing operational acoustic footprint.
Total Cost of Ownership (TCO)
While polyamides require precise engineering consideration regarding ambient moisture equilibrium and linear thermal expansion, their exceptional damping elasticity suppresses mechanical resonance. This protection shields steel driving shafts and gear trains from shock spikes, yielding a 3.4x mean time between failure (MTBF) enhancement.
Chinese Manufacturing Efficiency & Metallurgical Precision
Combining domestic vertical resin integration with proprietary automated horizontal casting and stress-relieving annealing ovens.
Anionic Polymerization Casting
Our MC (Monomer Cast) nylon billets utilize pure caprolactam monomer synthesized through precise alkaline catalysis. This achieves superior molecular mass (>100,000 g/mol) versus regular extrusion, delivering elevated modulus and thermal deflection limits.
Ultrasonic Void Elimination
Every nylon bar exceeding Ø50mm passes computerized immersion ultrasonic testing (UT). Rapid thermal quenching defects such as center-line shrinkage cavities and vacuum micro-porosity are methodically eliminated before export packaging.
Controlled Annealing Chambers
Internal stress leads to banana warping during asymmetric CNC machining. SHUNDA executes a 72-hour thermal oil or convection heat conditioning process, releasing frozen mechanical stresses to guarantee straightness down to 1.5mm/meter.
Integrated CNC Milling & Turning
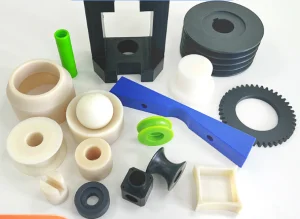
Beyond stock round rods, our factory floor operates multi-axis Mazak and Brother CNC machining centers. Importers source finished custom bush rings, helical gears, and wear sliders straight from raw material producers with zero intermediary markup.
Engineering Grade Comparison: Selection White Paper
Compare mechanical, thermal, and friction characteristics to engineer parts matched precisely to operating environments.
| Polyamide / Thermoplastic Grade | Tensile Strength (MPa) | Tensile Modulus (GPa) | HDT @ 1.8 MPa (°C) | Dynamic Friction (Dry) | Primary Industrial Use-Cases |
|---|---|---|---|---|---|
| Cast Nylon PA6G (Natural / Ivory) | 80 - 88 | 3.2 - 3.4 | 105 | 0.30 - 0.35 | High-tonnage crane pulleys, cable sheaves, gears, wear shoes, guide rollers. |
| MC Blue Cast Nylon (PA6G + Stabilizers) | 82 - 90 | 3.3 - 3.5 | 110 | 0.28 - 0.32 | General mechanical maintenance, food processing star wheels, quarry slides. |
| Oil-Filled Cast Nylon (Green PA6G+Oil) | 70 - 75 | 2.8 - 3.0 | 100 | 0.12 - 0.18 | High-speed unlubricated journal bearings, transmission bushings, marine rudders. |
| MoS2-Filled Cast Nylon (Black / Grey) | 85 - 92 | 3.5 - 3.8 | 115 | 0.22 - 0.26 | Heavy-load, slow-velocity open gears, valve guides, excavator slew bearing strips. |
| Glass-Filled Nylon (PA66-GF30) | 160 - 185 | 8.5 - 9.8 | 215 | 0.40 - 0.45 | Structural brackets, thermal breaks, pump impellers, automotive engine housings. |
| Acetal Copolymer (POM-C) | 65 - 70 | 2.8 - 3.0 | 95 | 0.25 - 0.28 | Precision timing cogs, medical valve plugs, dimensionally stable wet bushings. |
Mission-Critical Heavy Industry Applications
Engineered to absorb cyclic shock, damp acoustics, and eliminate surface galling across harsh operating conditions.
Heavy Lifting & Mobile Cranes
Precision-machined cast MC nylon sheaves reduce steel hoisting rope fatigue by dampening surface contact points. Extruded UHMWPE and PA6 outrigger pads provide load spreading on shifting soils, preventing catastrophic tip-overs on building sites.
Mining, Quarrying & Bulk Handling
Aggressive slurry, granite dust, and aggregate shred steel hopper plates. Our heavy cross-section nylon billets and liners combine high notched Izod resilience with natural lubricity, preventing sticky cake build-up and ensuring unimpeded material flow.
Hydraulics, Marine & Offshore
Subsea exposure rapidly oxidizes standard steel and bronze assemblies. Oil-filled nylon rudder pintle bearings and offshore winch spools eliminate grease washing while avoiding galvanic degradation across salty ocean conditions.
Global Sourcing Strategies: Overcoming B2B Supply Bottlenecks
How supply chain executives balance inventory velocity, quality control guarantees, and containerized logistics.
Consolidated Container Purchasing
Avoid managing half a dozen independent vendors for different polymer formulations. SHUNDA pairs nylon rods, tubes, and sheets alongside POM, ABS, HDPE, and UHMWPE into unified 20GP or 40HQ maritime shipments, minimizing customs brokerage fees and warehouse handling.
Moisture Stabilization During Transit
Polyamides absorb atmospheric humidity (up to 8-9% saturation). We hermetically seal machined components and stock billets in heat-shrunk polyethylene barriers accompanied by moisture desiccant bags, ensuring uncompromised roundness and dimensional stability across ocean voyages.
Traceable Quality Certifications
Every industrial shipment ships with mill test reports (MTR) verifying raw resin grade, density checks, tensile break limits, and hardness testing (Rockwell M / Shore D). We guarantee strict adherence to RoHS, REACH, and UL94 V-2 flammability ratings upon request.
High-Performance Cast Nylon, Composites & Polyolefins
Engineered profiles, oil-impregnated grades, and high-impact machine pads for severe heavy-duty deployments.








Technical & Commercial FAQ: Sourcing Nylon Rods
Key technical insights on nylon tolerances, thermal expansion, moisture uptake, and international ordering logistics.
What is the practical difference between Extruded PA6 and Cast MC Nylon (PA6G)?
Extruded PA6 is formed via screw extrusion under high pressure, making it well-suited for smaller rod diameters (Ø6mm – Ø100mm) with higher tensile flexibility. Cast MC Nylon (PA6G) relies on liquid monomer casting at atmospheric pressure. MC Nylon achieves a significantly higher molecular weight, superior compressive strength, and higher hardness (Rockwell M85 vs M75), and supports billets up to Ø800mm without internal thermal voids.
How does moisture absorption affect final CNC machined tolerances?
Unfilled Polyamide 6 absorbs 2.5% to 3.0% ambient moisture at 50% relative humidity, resulting in a dimensional expansion of approximately 0.2% to 0.3% per 1% of absorbed water. When machining precision tight-tolerance bushings (<0.05mm), we recommend conditioning stock prior to final cuts, accounting for dimensional growth, or specifying low-absorption alternatives like Polyoxymethylene (POM-C) or PA12.
How does SHUNDA ensure large diameter billets won't crack during deep turning?
Internal stress accumulation during rapid cooling is the primary culprit behind core cracking in large-diameter nylon rods. SHUNDA subjects all cast rods over Ø60mm to a secondary computer-controlled hot-oil annealing chamber for 48 to 72 hours. This process dissolves internal cooling strain, allowing aggressive asymmetric boring and deep broaching with minimal twist or fracture risk.
What cutting speeds and tool geometries are recommended for machining Nylon rods?
Polyamides have low thermal conductivity (approx 0.23 W/m·K) and low melting thresholds. High-speed steel (HSS) or polished carbide tooling with generous rake angles (15° to 30°) and clearance angles (10° to 15°) work best. Maintain sharp cutting edges and high feed rates (0.1 to 0.5 mm/rev) with active air-blast or water-soluble cooling to evacuate chips promptly and prevent frictional surface remelting.
Can you provide custom colors and additive fillers for specialized engineering requirements?
Yes. Beyond standard Natural (ivory) and Black, we regularly compound custom RAL/Pantone colors (Safety Blue, High-Visibility Yellow, Signal Red) alongside custom performance formulations, including 30% Glass Fiber Reinforcement (PA66-GF30), MoS2 Self-Lubricating, Internal Lubricant/Oil Fill, and Anti-Static ESD Conductive additives.
What are the standard order lead times and export ocean packing standards?
Standard rod diameters from Ø20mm to Ø200mm in Natural and Black are kept in buffer stock for immediate dispatch within 48 to 72 hours. Custom extruded or large cast runs typically ship within 10 to 15 business days. All export bundles are secured with heavy-duty moisture-proof PE wrap and packed inside reinforced fumigated wooden crates or steel-framed pallets designed for long-distance container transport.
Consult SHUNDA's Polymer Application Engineers
Send 2D/3D part drawings or specify raw rod stock requirements. Our engineering team reviews resin suitability, mechanical tolerances, and provides factory-direct wholesale pricing within 12 business hours.