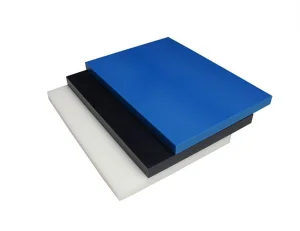
High-Performance Nylon Discs & Heavy-Duty Polymer Stock
Direct factory supply of precision-machined PA6, MC Nylon, and high-impact wear components built to strict industrial tolerances.






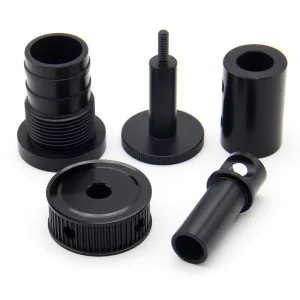

Engineering Evolution: The Role of Polyamide (Nylon) Discs in Modern Machinery
Deep technical insight into molecular morphology, stress-relaxation casting, and high-load mechanical damping.
In modern tribological and mechanical transmission systems, the Nylon Disc (Polyamide disc) has evolved from a generic plastic spacer into a critically calculated engineering component. Whether operating as heavy pile-driving hammer cushions, industrial rotary friction dampers, valve seats, or high-tensile drive discs, engineering-grade nylon delivers an unmatched synergy of viscoelastic impact absorption and dry lubricated wear resistance.
Standard metallic discs (such as bronze, ductile iron, or hardened carbon steel) subject surrounding mechanical frameworks to intense peak shock stresses. When subjected to repetitive cyclic concussive force—such as deep-foundation piling machinery—steel-on-steel interfaces accelerate metal fatigue, acoustic pollution, and micro-fissuring. Monomer Cast Nylon (MC Nylon / PA6G) discs eliminate these vulnerabilities through internal macromolecular slip, dampening up to 80% of secondary acoustic reverberation while sustaining extreme compressive yields exceed 110 MPa without brittle shatter.
Controlled Crystalline Polymerization
Our vertical vacuum-assisted anionic polymerization process increases polymer chain length, raising crystallinity to 48-52% compared to standard extruded polyamides (32-38%). This translates to higher surface hardness and superior dimensional stability under continuous thermal fluctuation.
Thermal Annealing & Stress Relief
Internal stress accumulation during casting is the #1 cause of circular disc warping during post-machining. Every SHUNDA nylon disc blank undergoes a computer-controlled 36-hour liquid thermal annealing cycle, mitigating radial residual stresses to less than 2.8 MPa.
Solid Lubricant Matrix Integration
For high-velocity friction discs, we homogenously disperse MoS₂ (Molybdenum Disulfide) and crosslinked synthetic lubricants directly into the liquid caprolactam before casting. This permanently drops the dry dynamic friction coefficient (µ) from 0.38 down to 0.16.
Material Engineering Reference: Polyamide Disc Variants
Selecting the precise polymer matrix according to mechanical shock, friction coefficients, and chemical immersion profiles.
| Material Formulation | Tensile Strength (MPa) | Izod Impact (kJ/m²) | Dynamic Friction (µ) | Core Application Environments |
|---|---|---|---|---|
| Cast PA6 (Natural White) | 85 – 92 | ≥ 6.5 | 0.32 – 0.38 | General machinery gears, guide wheels, wear washers, food-contact disc components. |
| Cast MC Nylon (Blue) | 90 – 98 | ≥ 7.0 | 0.28 – 0.34 | Heavy-load crane sheaves, excavator rotation rings, cable pulleys, structural flange spacers. |
| MoS²-Filled Nylon (Black Cushion) | 88 – 95 | ≥ 8.5 | 0.16 – 0.22 | Piling machine impact hammers, high-frequency continuous cyclic dampers, vibration isolation discs. |
| Oil-Impregnated Nylon (Green) | 75 – 82 | ≥ 6.0 | 0.12 – 0.15 | Unlubricated high-RPM thrust washers, industrial bottling lines, harsh marine conveyor discs. |
| Extruded PA66 | 80 – 85 | ≥ 5.0 | 0.35 – 0.40 | Small-to-medium diameter punched discs, electrical insulation gaskets, hydraulic seals. |
Enterprise Solutions Across Industrial Verticals
Deploying targeted nylon disc and engineering polymer systems to resolve uptime and wear challenges across four global sectors.
Deep Foundation & Piling Engineering
Impact cushion discs placed between pile-driving hammer rams and pile caps endure up to 3,000 kJ of raw force per stroke. Our cross-linked black nylon cushion rings prevent spalling of pre-cast concrete piles and protect diesel/hydraulic hammer rams from destructive rebound shockwaves.
Heavy Material Handling & Ports
Harbor container gantry cranes and mining conveyor belts utilize our large-diameter (up to 1,200mm) MC nylon guide discs and sheaves. Lightweight construction (1/7th the weight of steel) significantly reduces rotational inertia, cable fraying, and energy consumption.
Mining, Quarrying & Mineral Slurry
Abrasive slurry valves and cyclone separation units demand disc components that survive relentless scouring. Custom-machined PA6 and UHMWPE discs provide self-healing scratch resilience against quartz and granite fines, outlasting duplex stainless steel valves by 3.5x.
Automation & Robotic Actuation
High-speed planetary gear assemblies and rotary indexers require tight backlash control. Our precision CNC-milled nylon friction clutch discs and backlash-free spacers operate with zero chemical lubrication, preventing oil aerosol contamination in electronics and cleanroom facilities.
Technical Roadmap & Next-Generation Polymer Metallurgy
How SHUNDA is engineering tomorrow’s extreme-environment polymers through nano-reinforcement and eco-responsible lifecycle loops.
Carbon-Nanotube (CNT) Enhanced Nylon Discs
Targeted for release in 2026, our R&D facility in Hebei is pilot-testing multi-walled CNT dispersion within caprolactam monomer baths. Preliminary results demonstrate an electrostatic dissipative surface resistivity (≤ 10&sup6; Ω) and a 38% increase in heat deflection temperatures (HDT) at 1.8 MPa.
Hydrolytic Resistance Engineering
Polyamides naturally absorb ambient atmospheric water vapor (up to 7% under saturated immersion), resulting in radial swelling. Our novel chemical capping agent slows hygroscopic expansion by 65%, enabling offshore engineers to specify nylon discs in permanent submarine environments.
Closed-Loop Circular Machining Program
SHUNDA maintains complete post-industrial scrap segregation. CNC turning swarf from pristine natural nylon production is 100% remelted and chemically depolymerized back into pure monomer feedstocks, achieving a net 42% carbon footprint reduction for international sustainability audits.
Enterprise Supply Chain Integrity & Global Compliance
Export documentation, mill test certifications, and zero-defect quality assurance for Tier-1 OEMs worldwide.
Full EN 10204 3.1 Traceability
Every single consignment of wholesale nylon discs, rods, or cushions leaves our loading bay with a comprehensive chemical batch analysis, compressive modulus curve, and spectrophotometric color consistency report.
RoHS, REACH & FDA Certification
We supply natural unfilled PA6 disc variants that adhere strictly to FDA 21 CFR 177.1500 criteria for direct contact with foodstuffs, alongside full EU REACH Annex XVII compliance certifying zero restricted phthalates or SVHCs.
Heavy-Duty Maritime Export Crating
Nylon components are hygroscopic. We preserve precision tolerances during trans-oceanic shipping through vacuum-sealed aluminized moisture-barrier inner packaging inside ISPM-15 fumigated solid timber export crates.
Frequently Asked Questions: Nylon Disc Procurement & Machining
Authoritative technical answers to common queries submitted by industrial plant managers, procurement teams, and OEM engineers.
What is the primary mechanical difference between Cast Nylon (PA6G) and Extruded Nylon (PA66) discs?
Cast Nylon (PA6G) is synthesized directly from liquid monomer via mold polymerization under atmospheric pressure, enabling virtually unlimited disc diameters (up to 2000mm) and thickness with negligible internal molecular strain. Extruded Nylon (PA66) is formed via high-pressure mechanical extruders; it provides marginally higher tensile strength in thin disc profiles but suffers from significant internal orientation stress that tends to cause circular bowing when turning large disc diameters.
How do nylon hammer cushions perform in piling machines compared to Micarta, aluminum, or wood?
Traditional hardwood cushions split rapidly and pose fire risks, while aluminum discs work-harden and shatter under heavy cyclic blow counts. SHUNDA black-oil/MoS₂ nylon disc cushions absorb the sharp peak stress wave without mushrooming or brittle fracture, transferring optimal kinetic energy into the pile while maintaining hammer cycle life 4 to 6 times longer than composite fiber (Micarta) blocks.
How does SHUNDA compensate for moisture-induced hygroscopic dimensional change in nylon discs?
During engineering drawing review, our team calculates expected dimensional expansion based on your local ambient operating humidity or fluid contact. We either pre-condition the discs in high-temperature equilibrium water tanks before final CNC finishing, or machine critical bores and outside diameters to calculated "dry-to-wet" clearance allowances (±0.05mm).
Can you provide custom cut-to-size nylon disc blanks from cast plates or rods?
Yes. We operate multi-axis CNC routers, high-precision automated waterjet tables, and large-diameter turning lathes. We can slice circular disc blanks from cast nylon rods or machine them out of thick cast plates up to 200mm thickness, complete with counter-bored bolt holes, keyways, and lubrication spiral grooves.
What is the typical production and delivery lead time for wholesale custom nylon disc orders?
Standard diameter blanks (50mm to 500mm OD) held in stock ship within 48 to 72 hours. Custom formulated MC nylon castings or custom CNC turned components generally require 7 to 14 business days, supported by express air freight or consolidated ocean container logistics dispatched from Tianjin/Qingdao ports.
What drawing formats do your engineering and production departments accept?
Our CAD/CAM system accepts all universal 2D and 3D industrial interchange formats, including STEP (.stp), IGES (.igs), Parasolid (.x_t), SolidWorks (.sldprt), AutoCAD DWG, and vector DXF, as well as dimensioned PDF engineering drawings with defined ISO 2768-m or fine tolerances.
Comprehensive Engineering Polymers, Rods & Machined Stock
Explore our extended catalog of wear-resistant polymer shapes, PTFE, HDPE, and MC Nylon profiles engineered for global exporters.