Primary Polyolefin & Engineering Plastic Solutions
Directly sourced structural shapes and calibrated sheets designed for aggressive friction, impact, and chemical storage environments.







HDPE Sheet Manufacturing Trends & Next-Gen Polymers
Global infrastructure development, chemical processing, and sustainable material initiatives have revolutionized standard high-density polyethylene into a highly engineered, high-molecular matrix material.
High Molecular Weight Stabilization
The transition toward High Molecular Weight HDPE (HMW-HDPE) and Ultra-High Molecular Weight variations provides superior stress cracking resistance (ESCR) under persistent chemical immersion and dynamic cyclic loads.
Multilayer Co-Extrusion Technology
Modern manufacturing shifts toward multi-layer extruders capable of integrating functional UV absorbers, antimicrobial agents, or conductive antistatic carbon boundaries into specific functional zones without weakening core impact strength.
Controlled Annealing & Stress Relief
Eliminating internal mechanical stresses through calibrated secondary thermal annealing ovens ensures flat stock plates remain planar during multi-axis CNC routing, turning, and tight deep-hole drilling.
Industrial Grade Benchmark & Selection Matrix
International procurement teams must navigate trade-offs between tensile yield, continuous operating temperature, surface roughness, and friction coefficient. Compare our factory-calibrated specifications below.
| Physical / Mechanical Property | Test Standard | Standard Virgin HDPE (HD-300) | High-Molecular HDPE (HMW-500) | UHMW-PE (PE-1000 Grade) |
|---|---|---|---|---|
| Density / Specific Gravity | ISO 1183 / ASTM D792 | 0.955 - 0.960 g/cm³ | 0.950 g/cm³ | 0.930 - 0.940 g/cm³ |
| Molecular Weight Range | Gel Permeation / Viscosity | ~300,000 g/mol | ~500,000 g/mol | > 4,500,000 g/mol |
| Tensile Strength at Yield | ISO 527 / ASTM D638 | 28 - 32 MPa | 26 - 30 MPa | 20 - 24 MPa |
| Notched Izod Impact Strength | ISO 180 / ASTM D256 | 8 - 12 kJ/m² | 20 - 30 kJ/m² | No Break / >80 kJ/m² |
| Coefficient of Friction (Dynamic vs Steel) | ASTM D1894 | 0.20 - 0.25 | 0.18 - 0.22 | 0.10 - 0.15 |
| Continuous Operating Temp Range | DIN 53460 | -50°C to +80°C | -80°C to +85°C | -200°C to +80°C |
Chemical Process Tank Liners
Zero leaching and high resistance to aggressive acids, alkali solutions, and inorganic solvents make our continuous-roll and calibrated cut sheets optimal for galvanization baths and hydro-metallurgical scrubbing vessels.
Bulk Material Handling & Chutes
Engineered outrigger crane mats, drop chutes, dump truck bed liners, and silo hoppers take advantage of natural paraffinic wax release characteristics to completely eliminate material caking and cross-contamination.
Sanitary Food Cutting & Packaging
FDA and EU 10/2011 compliant material stock designed for meat cutting tables, poultry packaging guide tracks, conveyor star wheels, and wash-down machinery subject to daily caustic cleaning chemicals.
Worldwide Compliance & Factory Traceability
As a direct manufacturer and tier-1 supplier, we protect our international partners from import delays and out-of-spec deliveries through end-to-end certification and ruggedized oceanic packaging.
Batch Material Test Reports (MTR)
Every commercial production run includes EN 10204 3.1 certification detailing precise Melt Flow Index (MFI), density profiles, and tensile limits derived from calibrated laboratory stress testing.
Ocean-Freight Heavy Palletizing
Sheets are stacked on IPPC ISPM-15 fumigated solid wood or engineered composite pallets, bound with heavy PET tension banding, edge protectors, and moisture-barrier thermal PE shrink wrapping.
RoHS, REACH & Food Grade Safety
Raw materials are certified free from heavy metals, lead phthalates, bisphenol A, and SVHC chemical additives to ensure instant clearance in European, North American, and Australian ports.
Polyolefin Processing Roadmap & AI Integration
Continuous technical investments optimize energy profiles and dimensional tolerances, giving OEMs an edge in production yield and long-term operating costs.
AI-Calibrated Extruder Die Adjustments
Implementation of automated radiometric thickness scanners coupled with closed-loop thermal die bolts allows continuous sub-millimeter thickness corrections across the entire 2000mm extrusion width.
Circular Feedstocks & PCR Matrix Blends
Expanding dedicated co-extrusion streams that integrate up to 70% post-consumer ocean bound and post-industrial clean recycled resin into non-critical structural layers without compromising structural surface finish.
High-Speed Custom CAD/CAM Profiling
Equipped with 5-axis routers operating multi-tool carousels, our factory supplies pre-drilled, grooved, chamfered, and custom-beveled wear parts delivered ready for immediate line-assembly installation.
Frequently Asked Technical & Procurement Questions
Clear, direct answers to common engineering questions asked by project buyers, distribution partners, and manufacturing engineers.
For standard extruded sheets (thickness 1mm to 30mm), our calibrated roller calenders maintain ±0.15mm to ±0.3mm tolerance. Heavy compression-molded sheets (30mm up to 200mm) are precision surface-planed to achieve planar tolerances within ±0.5mm across standard 1220x2440mm and 1500x3000mm dimensions.
Due to non-polar surface energy (low dyne level), HDPE cannot be permanently bonded with traditional solvent adhesives or epoxy without dedicated flame/corona surface treatment. The industry standard method is hot gas extrusion welding or butt fusion using matched-melt HDPE welding wire, delivering joint tensile efficiencies exceeding 85%.
Virgin grade HDPE maintains maximum molecular chain integrity, yielding predictable Environmental Stress Crack Resistance (ESCR), higher tensile yield, and food safety certifications (FDA compliance). Recycled or blended sheets offer cost savings for non-critical drainage panels and flat ground protection mats, but exhibit lower elongation at break and higher brittleness below 0°C.
Standard natural (translucent white) and jet-black sheets carry a minimal MOQ of 500kg. Custom RAL or Pantone color masterbatch formulations require a 2,000kg run. Typical production run turnaround is 10 to 14 business days, with container staging at Tianjin or Qingdao ports within 48 hours of final QC clearance.
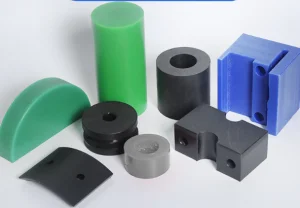
Engineered Polymers & Precision Extrusions
Expand your consolidated shipments with our complete range of ABS, POM, PP, and specialty co-polymer rods, tubes, and finished parts.