
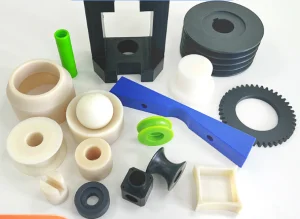
Primary Product Showcase
High-Performance Semi-Finished Stock & Custom Tubes
Engineered for extreme structural endurance, tight concentricity, and non-galling wear behavior in demanding mechanical assemblies.

OEM Engineering Plastic Backing Casting Board Nylon PP ABS PTFE UHMWPE Board Sheet Rod Tube
View Specifications
Cheap TEFLON Rod Manufacturers, Exporter
View Specifications
China Engineering Plastic Polyamide PA6 PA66 Nylon PP UHMWPE PTFE HDPE ABS Sheet Rod
View Specifications
MC Blue Cast Nylon Rod Plastic Round Rod And Bar
View Specifications
Impact Nylon Ring Cushion For Impact Hammer Piling Machines
View Specifications
Wholesale Natural MC Nylon Cast Rod Supplier, Company
View Specifications
Cheap Natural MC Nylon Sheet Factories, Exporters
View Specifications
Enterprise Solutions
High-Stress Engineering Scenarios: Why MC Pipe Dominates Metal Equivalents
Monomer Cast (MC) Nylon hollow bars and pipes represent a quantum leap over conventional extruded polyamides and bronze bearings. Designed to combat unlubricated friction, severe abrasive particulate ingress, and cyclical high-shock mechanical vibrations.
Heavy Lifting & Marine Crane Sheaves
MC nylon pipes machined into high-capacity wire rope pulleys preserve steel cables by absorbing boundary interface pressures, delivering up to 4x cable lifespan compared to cast iron or welded steel drums.
Hydraulic Cylinders & Piling Guide Sleeves
Engineered for extreme cyclical shock without plastic deformation. Self-lubricating MoS2 and oil-filled polymer blends prevent galling on chrome rods, even during lubrication starvation in sub-zero soil conditions.
Rotary Conveyor Bushings & Star Wheels
Zero electrolytic reaction and extreme chemical compatibility with cleaning acids and caustic washdowns. Reduces dynamic factory line noise by up to 15 dB compared to metallic roller and transmission interfaces.
Industrial Capability
China Smart Factory 4.0: Metallurgical Precision in Monomer Casting
Unlike standard screw-extruded nylon plagued by internal voids and cooling stresses, our Hebei manufacturing facility applies vacuum vertical centrifugal casting and computer-controlled liquid polymerization directly from caprolactam monomer.
Centrifugal Moulding
Eliminates air bubbles and density gradients. Dynamic rotational force guarantees superior crystalline density along the tube wall, enhancing peripheral wear performance.
Stress-Relief Annealing
Every semi-finished tube undergoes a proprietary 72-hour thermal cycle in oil tempering chambers. Prevents warping, cracking, or dimensional shift during subsequent deep CNC machining.
Near-Net Wall Sizing
Supplying optimized wall thicknesses from 15mm to over 200mm eliminates wasteful internal bore boring, cutting machine cycle time and material raw cost by up to 35% for tier-1 OEMs.
Integrated Traceability
Full batch identification from base caprolactam monomer lot numbers to finished ultrasonic non-destructive testing reports, supporting aerospace and defense documentation requirements.
Innovation Matrix
Technical Roadmap & Advanced Polymer Formulations
Meeting the demands of next-decade industrial mechanics through molecular modification, specialized tribological additives, and sustainable processing routes.
Phase I: Oil-Impregnated self-lubricating PA6G
Incorporating evenly dispersed liquid lubricating oil directly into the monomer formulation before casting. Lowers dynamic friction coefficient to μ=0.12, running maintenance-free without grease in inaccessible dry locations.
Phase II: High-Conductivity Anti-Static Nanotubes
Developing carbon nanotube-doped MC cast tubes for underground coal mining and offshore fuel-transfer pipelines. Surface resistivity tuned between 10^3 to 10^7 Ω prevents spark hazards under extreme flow velocity.
Phase III: Bio-Monamid Structural Blends
Pioneering green castor-derived dicarboxylic polymers within monomer casting lines to achieve a 40% reduction in Scope 1 & 2 embedded carbon footprint, meeting the rigorous European Carbon Border Adjustment Mechanism (CBAM).
Enterprise Procurement
Global Compliance, Rigorous QA & Supply Security
Navigating technical documentation and trade compliance without friction. We support engineers and procurement directors across Europe, the Americas, and the Asia-Pacific.
RoHS & REACH Compliance
Independently certified by SGS and TÜV. Free from heavy metals, phthalates, SVHC chemicals, ensuring frictionless market access for finished assemblies shipped into the EU and North America.
Export Protective Pack
Heavy-gauge moisture-barrier poly bagging, custom non-fumigation plywood crates, and end-cap protections ensure seamless transit without humidity warping or cosmetic scratching over ocean voyages.
Complete MTR Certificates
Material Test Reports (MTR) according to EN 10204 3.1 accompany every shipping lot, validating specific gravity, Rockwell hardness (M scale), elongation at break, and thermal deflection.
Agile Buffer Inventory
Offering dedicated vendor-managed stock for contracted high-volume clients. We warehouse pre-cast standard tubes ready for rapid 48-hour turnouts to maintain production continuity.
Technical Clarifications
Frequently Asked Engineering & Procurement Questions
Straightforward answers derived from 20+ years of direct workshop practice, CNC machining observations, and polymer testing.
What are the key performance differences between Extruded Nylon (PA6/PA66) and Monomer Cast MC Nylon Pipe?
MC Nylon (PA6G) is synthesized through an atmospheric anionic polymerization inside an open mold, resulting in a substantially higher molecular weight (up to 300,000–1,000,000 g/mol) and a crystalline content exceeding 45–50%, compared to 30–35% for extruded nylon. This molecular structure gives MC pipe higher tensile and compressive strength, elevated surface hardness, higher heat deflection temperatures (HDT), and drastically reduced residual internal stresses, making it far superior for high-tolerance CNC parts with large cross-sections.
How does MC Nylon pipe behave regarding moisture absorption and dimensional stability?
Like all polyamides, MC Nylon possesses polar amide groups that absorb atmospheric humidity (up to 6–7% at saturation in water immersion, or approximately 2% under ambient equilibrium). This water absorption plasticizes the polymer, improving impact resistance but reducing rigidity and expanding dimensions (typically 0.2% per 1% moisture absorbed). Where zero dimensional shift in wet operations is mandatory, we recommend POM (Acetal), UHMWPE, or our specially engineered oil-filled / glass-reinforced MC nylon grades.
What are the tooling and machining recommendations for precision CNC turning of MC pipes?
Use razor-sharp polished carbide or PCD tooling with large positive rake angles (15°–25°) and clearance angles of 10°–15° to prevent heat generation. Keep cutting speeds between 250 to 500 m/min with generous feed rates (0.15–0.4 mm/rev) to ensure material is cut cleanly rather than rubbed or smeared. Continuous chip extraction and pressurized air cooling are strongly advised over standard water-soluble coolant emulsions to prevent moisture absorption prior to final inspection.
Can SHUNDA manufacture custom colored, oil-filled, or MoS2-enhanced MC pipes?
Yes. In addition to standard natural ivory and blue MC nylon, our foundry routinely produces custom batches including: MC Black (MoS2-doped for improved surface lubricity and sliding resistance), MC Green (internally lubricated with synthetic oil for high-speed continuous motion), and custom RAL-matched colors for distinctive OEM corporate branding.
What is the standard turnaround time for OEM custom mold creation and production runs?
For custom outer/inner diameter combinations requiring dedicated tooling, we manufacture steel molds in-house within 5 to 7 working days. Initial pilot samples are delivered for dimensional sign-off via DHL/FedEx within 48 hours of casting. Volume serial production is typically completed and packed for container loading within 12 to 18 calendar days.
Complete Portfolio
Engineered Stock, Hollow Bars & Machined Bushings
Consolidate your procurement across polymers, structural boards, and certified heavy-duty sliding elements directly from our ISO-controlled workshop floor.

Nylon ABS PP PTFE Plastic Rod Tube Bar Roller
View Specifications
OEM Cast MC Nylon Rod Suppliers, Product
View Specifications
Cheap PTFE Sheet Supplier, Products
View Specifications
Impact Cushion For Impact Hammer Piling Machines
View Specifications
Cast Nylon Tube Rod Cast Nylon Pipe Bar MC Nylon Tube Bar
View Specifications
Cast PA6 Polyamide Nylon Plastic Tube Rod And Bar
View Specifications
MC Casting Nylon PA6 HDPE UHMWPE Sheet Hard Board
View Specifications