
Featured Engineering Polymer & Cushion Ring Products
Direct from our manufacturing base: heavy-duty piling hammer ring cushions, solid polymer bars, and wear-resistant sheets calibrated for demanding mechanical operations across North America, Europe, and Asia-Pacific.








Engineering Principles of Heavy-Duty Ring Rubber & Polymer Cushions
Modern infrastructure projects, heavy foundation engineering, and high-frequency hydraulic systems demand dynamic mechanical shock insulation that standard vulcanized rubbers cannot sustain. SHUNDA engineers hybrid elastomer composites and high-density polyamides to mitigate ultra-high peak shock waves.
Viscoelastic Dissipation & Energy Transfer
Ring rubber cushions and composite nylon pads installed on hydraulic impact hammers and piling rigs are subjected to compressive loads exceeding 450 MPa. Our micro-molecular compounding integrates high-rebound NBR, polyurethane, and cast PA6 polymers to maximize hysteresis loss, converting kinetic shock energy into controlled thermal dissipation rather than destructive structural fatigue.
- Shore Hardness calibration: 75 Shore A to 85 Shore D
- Minimized plastic deformation under cyclic impact
Acoustic & Stress Wave Attenuation
Foundation driving hammers produce acoustic pressure waves exceeding 115 dB, paired with intense rebound vibration that shatters internal metallic pistons. Our formulated ring cushions feature high internal damping ratios, attenuating peak acceleration spikes by up to 48%, protecting anvil surfaces, guide frames, and piling caps from premature micro-fracturing.
- Acoustic wave dampening conforming to ISO 3744
- Extended hammer lifespan by 3.2× over standard rubber
Thermal Stability & Chemical Inertness
Under non-stop operational cycles, localized heat accumulation within ring cushions can reach 120°C. Our compound matrix utilizes heat-stabilized synthetic elastomers blended with high-crystallinity cast nylon PA6, inhibiting thermo-oxidative degradation, oil washouts from hydraulic mist, and ambient chemical attack from marine salt spray and drilling bentonite slurries.
- Operating temperature range: -35°C to +135°C
- Hydrocarbon and ASTM oil swelling below 3.5%
Technical Roadmap & Next-Generation Material Horizons
As offshore wind foundations drill into ultra-deep basalt formations and industrial presses push hydraulic tonnage past 10,000 metric tons, the mechanical boundaries of standard elastomer and nylon rings are constantly redefined.
Graphene-Reinforced Elastomer Blends
Integrating nanoscale functionalized graphene oxide into the elastomeric base increases tensile shear yield by 34% while multiplying dynamic fatigue cycle thresholds, completely preventing ring split failures under asymmetric hammer blows.
Smart Sensor-Embedded Buffer Rings
Developing internal piezoelectric micro-sensors within heavy piling rings for real-time telemetry. Wireless transmission monitors compressive load distribution, internal thermal degradation, and predictive life cycles on offshore installation vessels.
Bio-Based Polyurethane Formulations
Formulating plant-derived polyols with aliphatic isocyanates to decrease cradle-to-gate carbon footprints by 42%, satisfying European ESG sustainability mandates without compromising mechanical resilience or tear strength.
Cryogenic Shore-D Self-Lubricating PA
MoS2 (Molybdenum Disulfide) and cross-linked silicone oil dispersed into cast PA6 formulations, achieving coefficient of friction below 0.08 while preserving extreme izod impact toughness down to -40°C in arctic offshore exploration.
Macro-Industry Solutions & Engineered Performance
Custom mechanical dampening and polymer seating designed to eliminate operational down-time across mission-critical infrastructure projects globally.
Deep Foundation & Civil Piling Rigs
During heavy sheet pile and pre-cast concrete post installation, hydraulic and diesel hammers strike the pile cap millions of times. SHUNDA impact nylon and composite ring cushions serve as sacrificial, ultra-durable shock buffers, guaranteeing uniform pile penetration velocity, eliminating pile head shattered concrete, and preserving the hammer ram's metallurgical integrity.
- High dimensional compliance: 300mm to 1800mm OD
- OEM fit for Junttan, IHC IQIP, Bauer & Delmag rigs
Offshore Wind Jacket & Monopile Drives
Offshore maritime foundation driving requires continuous, uninterrupted hammer impact sequences under extreme saline humidity and high surge resistance. Our sea-water proof black and blue nylon cushion rings prevent salt crystallization embrittlement, delivering predictable energy transfer coefficients for monopiles driving up to 80 meters subsea into dense seabed substrate.
- Hydrolysis-resistant polymer compounding
- High modulus retention under dynamic sea conditions
Heavy Hydraulic Presses & Mining Breakers
In aggregate quarry breakers and 5,000-ton forging presses, hydraulic backpressures cause catastrophic fluid seal extrusion and rod scoring. Our precision CNC-machined polyurethane, NBR, and POM buffer rings function as multi-stage dynamic sealing rings, withstanding high-pressure surges while dampening return stroke oscillations.
- Dynamic pressure threshold: Up to 700 bar
- Superior sliding resistance against abrasive micro-particles
China Factory 4.0: Supply Chain Resilience & Production Scale
Situated in Henglan Town, Xinhe County, Xingtai City, Hebei Province, SHUNDA operates a 35,000+ sqm vertically integrated production ecosystem combining monomer casting, precision profile extrusion, and multi-axis CNC finishing.
Vertical Feedstock Synthesis Control
Unlike downstream converting shops that purchase generic plastic rods, SHUNDA controls polymer polymerization in-house. From caprolactam monomer temperature-controlled reaction kettles to continuous casting ovens, every batch of MC Nylon and elastomer is tracked via digital DCS systems, ensuring zero voids, porosity-free cross sections, and unmatched internal density homogeneity.
Sub-Millimeter CNC Fleet
Equipped with 38 multi-axis CNC horizontal lathes, automated gantry milling centers, and laser ring-cutting fixtures, we machine custom inner/outer ring geometries, stress relief grooves, and chamfered sealing profiles within tight geometric dimensioning and tolerancing (GD&T) standards down to ±0.02 mm across diameters exceeding 1500 mm.
Export Packing & Supply Chain Redundancy
Strategically located near Tianjin and Qingdao deepwater ports, our supply chain guarantees high freight velocity. Finished ring cushions and polymer components undergo anti-UV shrink wrapping, desiccated vacuum boxing, and fumigated steel-bracket wooden crating, preventing moisture absorption or warping across multi-week ocean transit cycles.
Engineering Polymer & Cushion Matrix for Procurement Officers
Compare mechanical metrics across primary polymer grades to ensure accurate procurement specifications based on peak compressive loading, environmental chemistry, and tribological constraints.
| Material Classification | Tensile Strength (MPa) | Compressive Yield (MPa) | Shore Hardness | Continuous Temp (°C) | Primary Industrial Role | Industry Standard |
|---|---|---|---|---|---|---|
| Cast MC Nylon (PA6) | 85 – 110 | 115 – 140 | 82 – 88 Shore D | -40 to +110 | Piling hammer cushions, heavy sheaves, buffer rings | DIN EN ISO 527 |
| Polyurethane (Cast CPU) | 45 – 65 | 80 – 105 | 70 – 95 Shore A | -30 to +90 | Flexible hammer cushions, shock boots, rod wipers | ASTM D412 |
| POM (Acetal Copolymer) | 65 – 82 | 90 – 115 | 80 – 85 Shore D | -50 to +105 | Precision hydraulic guide rings, valve seals, bushings | ISO 9988 |
| UHMWPE (Ultra High Molecular) | 35 – 48 | 30 – 45 | 62 – 68 Shore D | -150 to +80 | Wear guide plates, low friction marine fender liners | ASTM D4020 |
| NBR / Synthetic Rubber | 14 – 22 | 25 – 40 | 60 – 85 Shore A | -35 to +125 | Oil-resistant O-rings, pipe cushion rings, flange seals | ASTM D2000 |
| PTFE (Virgin / Carbon Filled) | 22 – 38 | 15 – 25 | 55 – 60 Shore D | -200 to +260 | Extreme acid/alkali backing rings, dynamic rotary seals | DIN 53455 |
Localized Engineering Support & International Compliance
Procuring engineering components overseas requires absolute certainty regarding material certifications, environmental conformity, and total cost of ownership (TCO) predictability.
Rigorous QA & 3.1 Material Certifications
Every shipment leaving our Hebei factory is accompanied by EN 10204 3.1 inspection certificates, non-destructive ultrasonic void testing reports, and batch density validations. Our metrology laboratory maintains CMM (Coordinate Measuring Machines) and Shore hardness testers cross-calibrated against global laboratories.
- ISO 9001:2015 certified quality management
- Full traceability back to polymer synthesis lots
EU & US Regulatory Compliance
Our raw resins and vulcanized elastomer formulations comply strictly with RoHS Directive 2011/65/EU and REACH (EC 1907/2006) Substance of Very High Concern (SVHC) regulations. For food contact equipment and clean municipal water systems, specific grades are supplied fully compliant with FDA 21 CFR 177.1500 standards.
- Zero heavy metal plasticizers or banned Phthalates
- REACH SVHC testing validated through SGS/TUV
TCO Optimization & Field Economics
By switching from domestic middleman distribution to factory-direct engineered cushions, global piling contractors achieve 35% to 55% direct procurement cost reductions. More crucially, our wear-resistant formulation reduces cushion stack replacement frequencies by up to 2.8×, slashing crane operational downtime costs.
- Average field replacement savings: $18,000/rig/year
- Guaranteed dimensional stability across 100,000 blows
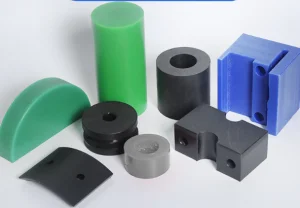
Industrial Rods, Tubes & Machined Structural Components
Complete engineering inventory ready for immediate container dispatch or precision CNC machining according to customer blueprints and CAD models.







Frequently Asked Questions for Engineering & Procurement Specialists
Answers addressing material formulation, lifecycle comparisons, custom manufacturing tolerances, and international logistics.
What distinguishes MC Cast Nylon ring cushions from conventional natural or NBR rubber rings in piling operations?
While standard vulcanized rubber rings exhibit high elastic deflection, their ultimate compressive yield strength is typically capped below 35 MPa. Under modern high-energy hydraulic hammers (rated at 50 kNm to 500+ kNm), rubber rings deform plastically, build excessive hysteresis heat, melt, or experience catastrophic blowout fractures within hundreds of blows.
SHUNDA Monomer Casting (MC) Nylon PA6 ring cushions offer compressive strengths up to 135 MPa paired with controlled viscoelastic memory. They transmit the necessary peak driving force into the pile while filtering out high-frequency reflective tension waves, lasting 4 to 8 times longer than pure rubber or timber cushion stacks.
Can SHUNDA fabricate hybrid elastomer-bonded polymer ring cushions?
Yes. We manufacture layered composite cushion assemblies consisting of alternating discs of cast PA6 nylon and high-rebound polyurethane or NBR elastomer vulcanized with structural primers or mechanically nested with interlocking locating rings. This hybrid configuration combines the high impact attenuation of softer rubber with the high mechanical load-bearing capacity of engineering polyamide.
What dimensional range and manufacturing tolerances can your CNC factory support?
We cast and machine solid rings, hollow sleeves, and split buffer rings with Outer Diameters (OD) spanning from 50 mm up to 2200 mm, with wall thicknesses up to 250 mm. Our high-precision CNC turning lathes hold tolerances within ±0.05 mm on standard diameters and down to ±0.02 mm on precision ground sealing grooves, completely stress-relieved via annealing cycles to ensure zero ovalization or dimensional drift post-machining.
How does ambient temperature and marine environmental exposure impact your ring cushion life?
Standard commercial polyamides are prone to moisture absorption, which softens the material and can induce dimensional expansion in wet offshore work. To counter this, SHUNDA incorporates oil additives, stabilizers, and specialized co-polymerizers that reduce ambient moisture uptake below 1.2% (compared to 6-8% in commodity PA6). Our polymers are chemically inert to diesel exhaust residue, drilling foams, hydraulic oils, and saline sea immersion across continuous temperatures from -40°C to +110°C.
What is the standard production lead time and quotation dispatch turnaround for overseas buyers?
Our multilingual technical sales engineering team provides official quotations, material datasheets, and engineering recommendations within 12 hours of inquiry submission. Prototype or sample ring cushions are dispatched within 3 to 5 business days, while standard 20ft/40ft container production orders are typically fulfilled within 12 to 18 calendar days, backed by our extensive stock of semi-finished billets.
Request Custom Polymer & Ring Rubber Engineering Quotes
Whether replacing worn-out OEM piling cushions, designing specialized subsea dynamic seals, or sourcing bulk semi-finished engineering polymers direct from China's primary manufacturing belt, our engineering team is ready to evaluate your CAD models, material requirements, and operational parameters.