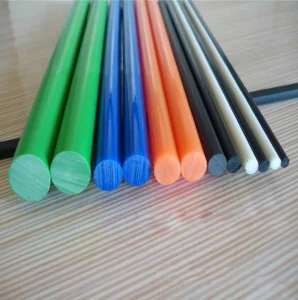
High-Performance Nylon Stock & Semi-Finished Shapes
Explore our foundational range of virgin polyamides, extruded PA6/PA66 boards, cast hollow tubes, and custom alloyed stock engineered for superior structural integrity.








Evolutionary Trends in High-Performance Nylon Boards
Polyamides have transitioned from basic metal replacement to mission-critical composite matrices. As heavy machinery, electric mobility, and clean industrial processes accelerate, nylon board manufacturers face stricter demands for mechanical reliability.
Additive-Enhanced Tribology
Modern applications favor self-lubricating nylon boards infused with MoS₂ (Molybdenum Disulfide), solid lubricants, and nano-oil additives. This reduces dry-run friction coefficients below 0.15, eliminating maintenance shutdowns in conveyor drives, telescopic boom slide blocks, and maritime winch assemblies.
Stress Relief & Cryogenic Annealing
Residual inner tension often leads to warped boards during rapid CNC routing. Leading companies have adopted computerized secondary post-cure annealing cycles that guarantee dimensional flatness across boards exceeding 100mm in cross-section thickness.
Hydrolytic & Thermal Stabilization
By blending PA6/66 chains with advanced heat stabilizers, modern nylon plates maintain mechanical stiffness under sustained 120°C continuous working environments, preventing premature embrittlement and catastrophic yield under cyclical torque.
Engineering Selection Matrix: Nylon Boards vs. Alternative Polymers
Choosing the correct polymer substrate dictates total equipment operational life (MTBF). Our engineers have systematized key mechanical differences to guide precision procurement.
| Polymer Variant | Tensile Strength (MPa) | Dynamic Friction Coeff. | Moisture Saturation (23°C) | Core Application Suitability | Form Availability |
|---|---|---|---|---|---|
| Cast Nylon PA6G (Natural/Blue) | 80 - 85 | 0.20 - 0.28 | 6.0% - 7.0% | Heavy sheaves, crane outrigger pads, large wear strips | Sheets 5-200mm Custom Rods |
| Extruded PA66 | 85 - 90 | 0.25 - 0.32 | 8.0% - 8.5% | High-temperature fasteners, electronic structural panels | Boards Round Bars |
| Oil-Filled / MoS₂ Nylon | 72 - 78 | 0.12 - 0.18 | 5.5% - 6.0% | High-speed gear wheels, autonomous conveyor tracks | Machined Parts Plates |
| POM-C (Polyacetal Acetal) | 65 - 70 | 0.25 - 0.30 | 0.8% - 1.0% | Precision dimensional valves, submerged water guides | Rods Sheets |
| UHMWPE | 22 - 35 | 0.10 - 0.15 | < 0.01% | Zero-moisture bulk liners, chemical chute skirts | Sheets Profiles |
Impact Shock Attenuation
Unlike brittle metals or non-reinforced thermoplastics, monomer cast nylon exhibits outstanding viscoelastic damping. Under seismic impact or recurring drop-hammer cycles, cast PA plates absorb mechanical kinetic shock, preserving hydraulic actuators.
Weight Reduction Mechanics
With an average specific density of 1.15 g/cm³, nylon boards weigh approximately 1/7th the weight of bronze or steel. This reduction decreases inertial drag in high-speed rotary packaging equipment while drastically reducing power consumption.
Chemical Resistance Matrix
Resistant to organic solvents, hydrocarbons, esters, ketones, and common industrial oils. Nylon boards act as non-corrosive chemical barriers in alkaline washing plants, electroplating tracks, and industrial effluent transfer facilities.
Cross-Industry Engineering Solutions
From deep-sea drilling derricks to clean automated pharmaceutical distribution hubs, high-grade polyamide boards form the backbone of wear prevention.
Heavy Construction & Cranes
Engineered outrigger pads, telescopic boom wear shoes, cable guide sheaves, and vibration isolating foundations prevent premature wear on structural steel girders.
Intralogistics & Conveyance
Low-noise curve tracks, chain guides, star wheels, and divert arms maintain zero-scuff handling on delicate bottling and automated package sorting lines.
Bulk Materials & Mining
Impact cushion rings for piling equipment, drop chutes, hopper discharge liners, and slurry scraper blades prevent wet ore bridging and steel abrasion.
Maritime & Hydro Engineering
Sluice gate bushings, underwater rudder bearings, dock bumper wear surfaces, and mooring winch spools endure corrosive salt spray without galling.
Global Enterprise Standards & QA Protocols
SHUNDA couples direct-from-mill production with international traceability to safeguard supply continuity for Tier-1 OEMs and distributors.
Raw Material Integrity
Every single batch of polyamide is compounded using 100% virgin caprolactam without unclassified scrap additives. Mill test reports (MTR) including density, elongation at break, and hardness are delivered with each shipment.
12-Hour Engineering Response
Our dedicated bilingual application engineering desk operates across multiple time zones. Inquiries containing CAD, STEP, or DXF files receive complete toolpath feasibility reviews and cost modeling within 12 business hours.
Export-Grade Protection
Machined nylon items and full-size boards are hermetically sealed in multi-layer moisture barrier foils and reinforced solid-wood crates to eliminate environmental moisture pick-up during deep-ocean transit.
Next-Generation Polymer Roadmap & Sustainability
Anticipating the demands of clean manufacturing, smart factories, and circular material flows over the coming decade.
Bio-Based Polyamides
Advancing monomer synthesis derived from renewable castor oil derivatives (PA1010 / PA11 / PA610) to reduce embedded carbon footprints by up to 45% without sacrificing tensile yield or wear endurance.
IoT-Embedded Smart Wear Plates
Co-extruding conductive nano-carbon strips into critical wear zones. This allows real-time structural health monitoring, broadcasting wireless early-warning signals before guide boards wear through to costly metal drive wheels.
Closed-Loop Precision Regrind Recycling
Expanding closed-loop clean swarf reprocessing infrastructure to convert high-purity CNC machining shavings into non-critical auxiliary structural shapes, directly supporting global scope-3 carbon reduction targets.
Frequently Asked Questions on Nylon Boards & Machining
Clear, authoritative answers directly compiled by our manufacturing metallurgical and polymer specialists.
What are the definitive differences between Cast Nylon (PA6G) and Extruded Nylon (PA66)?
Cast Nylon (MC PA6G) is produced via liquid monomer anionic polymerization inside pressure-free molds. This allows virtually unlimited cross-sectional thickness (up to 200mm+) with minimal internal stress, superior wear resistance, and higher crystallinity. Extruded Nylon (PA66) is forced through an extrusion die under high mechanical pressure, offering slightly higher tensile rigidity and heat resistance in smaller profiles, but is subject to higher internal shear stress if not meticulously annealed.
How do you control dimensional tolerances given nylon's natural hygroscopic nature?
Polyamides absorb ambient moisture (up to 6-8% at complete equilibrium saturation), which expands linear dimensions roughly 0.2% per 1% moisture gain. We counteract this by precision-machining dry, stress-relieved blanks with pre-calculated moisture expansion offsets. Alternatively, for submerged or humid environments requiring tighter tolerances than ±0.05mm, we advise specifying our POM (Acetal) or MoS₂/Oil-impregnated grades.
Can SHUNDA produce custom CNC milled and turned parts directly from CAD files?
Yes. Our in-house machine center operates high-speed multi-axis CNC routers, lathes, and mill-turn centers tuned explicitly for engineering polymers. You can upload STEP, IGES, DWG, or PDF drawings. Our production engineers verify clamping dynamics, tool cooling sequences, and deliver 100% finished components ready for assembly line insertion.
What are the lead times for custom-cast oversized nylon sheets and cut blocks?
Standard thicknesses of natural white and blue cast nylon boards (10mm to 100mm) are held in ready stock for swift dispatch within 3–5 working days. Specialized alloyed formulas (oil-filled, graphite, carbon-fiber reinforced, or custom RAL colors) typically require 10–14 working days for casting, oven-annealing, precision skimming, and export seaworthy crating.
Precision Finished Components, Profiles & Alloyed Plates
Complete your supply chain requirements with customized pads, wear-resistant hammer rings, high-lubricity fluoropolymers, and polyolefin solutions manufactured to exact standards.