
Primary Extruded Rods & Monomer Casting Profiles
Engineered for high-yield machinability, dimensional stability, and stringent tribological environments. Explore our top factory-direct product range.


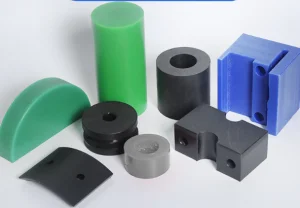
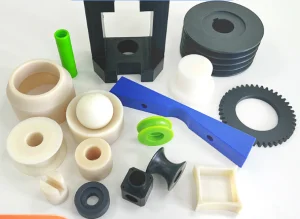



Engineering Fundamentals: Polymer Dynamics in Rod Extrusion
Understanding the interplay between thermal shear rheology, crystalline orientation, and vacuum sizing calibration is essential for procuring industrial extruded stock that will not warp or fracture during multi-axis CNC turning.
Extrusion vs. Casting Crystallinity
Continuous extrusion aligns polymer chains along the drawing axis, providing outstanding flexural resistance and uniform radial shear. By contrast, Monomer Casting (MC Nylon) utilizes horizontal or vertical chemical polymerization, optimizing core molecular weight for extreme compressive load ratings without thermal melt fatigue.
Thermal Rheology & L/D Screw Design
High-grade rod manufacturing utilizes high Length-to-Diameter (L/D > 32:1) barrier screws with modulated compression ratios. This eliminates thermal degradation in sensitive resins such as Polyoxymethylene (POM Acetal) and avoids melt fracture while delivering an ultra-dense, homogeneous cross-section.
Deep-Cycle Stress Relief Annealing
Internal stresses formed during water-bath cooling cause catastrophic warping when cutting keyways or boreholes. High-specification extruded rods undergo programmable multi-stage air/oil bath annealing for up to 48 hours to fully normalize crystalline morphology and lock in absolute geometric stability.
Engineering Polymers Specification & Machinability Guide
A rigorous property cross-reference formulated by our chemical engineers to guide global sourcing specialists in matching operational loads to optimal polymer chemistry.
| Polymer Classification | Tensile Strength (MPa) | Operating Temp Range (°C) | Coefficient of Friction (μ) | Moisture Saturation (24h %) | Primary Industrial Vector |
|---|---|---|---|---|---|
| PA6 / MC Cast Nylon | 75 - 85 | -40 to +110 | 0.25 - 0.35 | 1.8% - 2.2% | Crane sheaves, heavy gears, earthmoving impact cushions, guides |
| POM-C (Polyacetal Copolymer) | 65 - 72 | -50 to +105 | 0.20 - 0.28 | 0.2% | High-precision gears, fluid manifolds, tight-tolerance valves, sprockets |
| UHMWPE (Ultra-High MW) | 35 - 45 | -150 to +85 | 0.10 - 0.15 | < 0.01% | Chute wear liners, cryogenics, conveyor tracking strips, marine fenders |
| PTFE (Polytetrafluoroethylene) | 22 - 32 | -200 to +260 | 0.04 - 0.08 | < 0.01% | Aggressive chemical seals, semiconductor valve stems, high-dielectric isolators |
| PEEK (Polyetheretherketone) | 100 - 115 | -60 to +250 | 0.30 - 0.38 | 0.1% | Aerospace back-up rings, medical autoclave brackets, downhole oil/gas seals |
| ABS / High-Impact PP | 30 - 45 | -20 to +80 | 0.30 - 0.40 | 0.3% - 0.7% | Galvanic electroplating tanks, lightweight rapid structural prototyping |
China Factory 4.0: Supply Chain Resilience & Processing Efficiency
How state-of-the-art Chinese extrusion infrastructure combines upstream petrochemical integration, automated line closed-loop calibration, and end-to-end quality controls to deliver undeniable global procurement value.
Gravimetric Feeding & Dehumidification
Processing engineering plastics begins in closed-loop molecular sieve dryers. Our automated lines precisely regulate polymer moisture content to below 0.02% before melt plasticization, effectively eliminating microporosity, air pockets, and hydrolysis-induced chain scission.
Inline Ultrasonic Flaw Detection
Critical engineering rods destined for high-speed dynamic machining pass through multi-point online ultrasonic scanners. Sub-surface void anomalies, vacuum cavities, or center-line shrinkage flaws are detected instantly, preventing defective stock from ever leaving the plant.
Complete Integrated Cluster Resilience
Situated in the heart of Hebei’s manufacturing corridor, SHUNDA integrates virgin monomer polymerization, precision extrusion tooling fabrication, custom color masterbatch compounding, and 5-axis CNC machining centers into a unified single-site logistics hub.
Macro-Industry Solutions Across Global Value Chains
From heavy infrastructure civil engineering to micro-fluidic semiconductor cleanrooms, our extruded rods and tailored components replace metals to eliminate lubrication, resist corrosion, and reduce overall equipment deadweight.
Heavy Construction & Piling
High-energy impact cushions machined from specialized cast MC polyamide absorb multi-ton pile-driver shockwaves, protecting hammer anvils and concrete pilings while delivering up to 300% longer operating life than conventional hardwood or phenolic composites.
Automated Material Handling
Extruded UHMWPE and POM-C profiles serve as high-speed conveyor slide tracks, star wheels, and sprockets. Their whisper-quiet operation, ultra-low friction coefficient (μ < 0.15), and self-lubricating characteristics drastically cut electric motor drive loads.
Food, Beverage & Pharma Processing
FDA-compliant natural virgin polyoxymethylene and UHMWPE round rods feature ultra-dense non-porous surfaces that resist high-pressure caustic steam and CIP washdowns, eliminating the risk of bacteriological harboring and microplastic detachment.
Renewable Energy & Marine Engineering
Corrosion-proof marine fender bushes, pivot bearings, and wind-turbine yaw slide pads forged from oil-impregnated MC nylon withstand continuous saline exposure, high-amplitude vibrations, and zero-maintenance subsea conditions.
Semiconductor & Electronics
Extruded PTFE and high-purity PEEK rods maintain structural dielectric isolation under continuous thermal stress up to 250°C. Extremely low trace ionic impurities and ultra-low outgassing guarantee high yields in ultra-clean wafer-processing chambers.
Fluid Handling & Petrochemical
Corrosion-proof valve balls, metering stems, and acid-resistant tank flanges fabricated from virgin PP and PVDF extruded rods withstand continuous exposures to aggressive inorganic acids, aromatic solvents, and high-temp alkaline mixtures.
Global Enterprise Sourcing: TCO, Risk Mitigation & Precision Tolerancing
A strategic purchasing roadmap designed for supply chain vice presidents and procurement directors balancing unit costs, CNC turning scrap rates, and international shipping lead-time security.
Total Cost of Ownership (TCO) vs. Raw Material Price
Purchasing sub-standard, un-annealed plastic rods yields high initial margins but explodes final scrap rates. Centerline voids, internal stress banana-curving during high-speed CNC turning, and inconsistent hardness directly cause carbide tool chatter, dimensional rejections, and line shutdowns. SHUNDA’s zero-stress rods guarantee near-zero machining scrap.
Export-Grade Vapor-Proof Preservation Packaging
Polyamides (Nylon PA6 and PA66) are naturally hygroscopic, absorbing up to 8% atmospheric moisture when exposed to maritime container microclimates. This alters rod diameters and induces premature hydrolytic swelling. We ship all precision rods packed in vacuum-sealed aluminum-foil moisture barriers with desiccants on heavy-duty fumigated wooden pallets.
Tolerance Standards: DIN 16980 & ISO 2768-m
Every extruded rod is calibrated via vacuum-immersion sizing sleeves, ensuring strict compliance with DIN 16980 and ISO 2768-m outer diameter tolerances. Surface finish meets Ra ≤ 1.6 μm, minimizing pre-turning skim cuts and maximizing material recovery in automatic Swiss-type screw machining centers.
Dual-Track Sourcing & Rapid JIT Buffer Stock
To insulate global OEMs against freight fluctuations, SHUNDA provides contractual consignment inventory and continuous regional buffer-stock systems. Standard sizes of nylon, POM, and UHMWPE rods can be dispatched to global container hubs within 48 hours of order clearance.
Technical Roadmap: Next-Generation Polymer Extrusion Frontiers
Pioneering advancements in nanoparticle composites, self-sensing polymers, and closed-loop bio-circular engineering designed to reshape industrial product life cycles over the coming decade.
Nanotube & Graphene Fillers
Integrating surface-treated carbon nanotubes (CNTs) and graphene nanoplatelets into polyamides and acetal resins yields structural rods with enhanced tensile modulus (+45%), superior thermal conductivity, and permanently uniform electrostatic dissipation (ESD 10^6 - 10^9 Ω).
Advanced Tribological Solid Lubrication
R&D compounds integrating fluoropolymer micro-powders, molybdenum disulfide (MoS2), and cross-linked silicone matrices directly into the melt stream. The resulting extruded components operate with zero dry-running stiction and achieve dramatic 4-fold decreases in counter-surface steel shaft wear.
Closed-Loop Bio & Chemically Recycled Resins
Achieving carbon neutrality demands verified material lifecycle governance. SHUNDA is leading trials of depolymerized, chemically recycled caprolactam monomer feedstocks and bio-based castor oil polyamides (PA11/PA610), delivering 100% virgin-equivalent mechanical properties with >60% lower carbon footprints.
Regulatory Compliance, Traceability & Local Engineering Support
Our commitment to rigorous regulatory compliance protects OEM supply chains against cross-border customs seizures, environmental liabilities, and field recall risks.
RoHS 3 & REACH SVHC Strict Compliance
Every polymer batch is third-party certified by SGS/TUV testing agencies against EU RoHS Directive 2011/65/EU and REACH Candidate List of Substances of Very High Concern (SVHC). Guaranteed zero heavy metals, phthalates, PFOA/PFOS, or halogenated flame retardants.
FDA 21 CFR & EU 10/2011 Food Contact
Our natural POM, virgin PE, and food-grade nylon resins comply fully with US FDA 21 CFR 177 standards and European Regulation (EU) No 10/2011 for repetitive food-contact applications, verified through migration testing in aqueous, acidic, and fatty food stimulants.
EN 10204 3.1 Traceability & Batch COA
All bulk deliveries are accompanied by EN 10204 Type 3.1 Material Test Certificates and traceable batch QR codes. From the virgin monomer lot number through melt temperature logs to final optical micrometer inspection, complete historical traceability is preserved for 10 years.
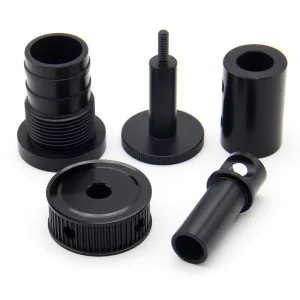
Precision Fabricated Sheets, Specialty Pads & Custom CNC Assemblies
Complementing our core extruded rod lines: high-molecular plates, custom CNC turned components, and heavy industrial wear pads engineered to international CAD/CAM drawings.






Frequently Asked Technical & Procurement Inquiries
Detailed engineering explanations answering critical questions raised by chief mechanical engineers, tooling managers, and global polymer buyers.
What causes centerline porosity in large-diameter extruded acetal (POM) rods, and how does your factory prevent it?
When should an engineer specify Cast MC Nylon instead of Extruded PA6 or PA66 round rods?
How do you manage moisture absorption and dimensional stability during overseas container transit?
What are the exact recommended cutting speeds, rake angles, and tooling for CNC turning extruded plastic rods?
Can SHUNDA synthesize custom filled or color-matched extruded engineering rods?
What standard certifications and analytical QA reports accompany every production shipment?
Initiate Your Custom Extruded Rod Specification
Send our senior plastics engineers your 2D/3D component drawings, target operating loads, chemical exposure conditions, and annual blanket purchase volumes. We guarantee a thorough technical review and competitive DDP/FOB quotation within 12 business hours.