

OEM Plastics Polyamide Natural Mc Nylon Cast Nylon PA6 Rod Round Bar Engineering Plastic Polyamide PA6 PA66 POM Nylon PP UHMWPE PTFE HDPE ABS Plastic Rod And Bar Manufacturer, Company
View Specifications
Explore our certified stock inventory of polyamide, polyoxymethylene, and advanced fluoropolymer shapes manufactured for tight-tolerance CNC routing, milling, and turning.






An in-depth analysis of monomer casting technology, high-load mechanical dynamics, and weight-reduction imperatives shifting modern industrial mechanical design.
Unlike standard extruded polyamide (PA6 extrusion), Cast Nylon (MC Nylon) is synthesized via an anionic ring-opening polymerization of caprolactam directly within precision temperature-regulated molds. This atmospheric pressure casting process produces an exceptionally high molecular weight (300,000 to 500,000 g/mol) and a superior crystallinity level exceeding 45%, providing outstanding compressive strength and resistance to plastic deformation under continuous cyclical loads.
Global original equipment manufacturers (OEMs) across mining, maritime, and automation industries are actively executing bronze and steel replacement initiatives. Cast sheet plastics offer one-seventh the weight of bronze (density ~1.15 g/cm³ vs 8.8 g/cm³), substantial vibration damping properties (reducing decibel ratings up to 10 dB in gear trains), zero risk of galvanic corrosion, and dry-running capabilities that eliminate lubricating grease contamination.
The principal failure mode in precision plastic CNC machining is warp and dimensional drift induced by unresolved internal stresses. SHUNDA implements a computerized dual-stage liquid heat-treatment annealing cycle. Raw cast plates undergo controlled ramp-up, soaking at peak glass transition ranges, and a prolonged multi-day cooling stage. This removes residual stress fields, ensuring plate flatness of under 0.5 mm/m after high-speed milling.
Review engineering parameters established according to ISO 527, ISO 178, and ASTM test protocols to guide component design and material certification.
| Polymer Classification | Tensile Strength (MPa) | Flexural Modulus (GPa) | Impact Strength (kJ/m²) | Max Operating Temp (°C) | Primary Industrial Role |
|---|---|---|---|---|---|
| Cast Nylon PA6 (Natural/Blue) | 85 – 95 | 3.2 – 3.5 | Charpy Unnotched: No Break | 105°C (Short: 160°C) | Heavy-duty sheaves, crane outriggers, massive sprockets, friction guides |
| POM-C (Polyacetal Copolymer) | 65 – 72 | 2.8 – 3.0 | Izod Notched: 6.0 | 100°C (Short: 140°C) | Precision gears, fluid manifolds, tight-tolerance electrical switchgear |
| UHMWPE (PE-1000 Grade) | 22 – 30 | 0.7 – 0.9 | Double Notched: 110+ | 80°C (Short: 100°C) | Bulk hopper drop chutes, conveyor wear strips, port fender facing |
| PTFE (Virgin / Carbon Filled) | 25 – 35 | 0.6 – 0.8 | Izod Notched: 16 | 260°C (Continuous) | Cryogenic seals, aggressive chemical valve seats, non-stick thermal pads |
| High-Impact ABS Plate | 42 – 48 | 2.1 – 2.4 | Izod Notched: 18 | 75°C (Short: 90°C) | Thermoformed equipment shrouds, structural casings, automotive dashboards |
How SHUNDA integrates polymer chemistry, captive mold manufacturing, and precision multi-axis CNC routing under one audited operational infrastructure in Xinhe County, Hebei.
Situated in the heart of Hebei’s industrial heartland, our plant leverages instant raw caprolactam monomer and chemical masterbatch availability, drastically decreasing resin freight cost and production cycles compared to overseas suppliers.
Custom plate dimensions, thick-section slabs up to 250 mm, or custom circular molds are engineered in our captive mold shop. This enables quick prototype turnarounds in days rather than waiting weeks for outside tooling houses.
Avoid double-handling markups. Our machining bays include high-speed gantry routers, multi-axis vertical machining centers, and live-tooling lathes configured specifically for engineering plastics, running chip extraction and non-contaminating dry coolant.
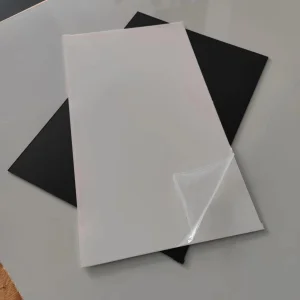
Sheets and machined parts are coated with anti-scratch protective poly-masking, packed with moisture-absorbing desiccants, banded onto heat-treated ISPM-15 export wooden pallets, and boxed in sturdy plywood containers for damage-free maritime freight.
Verified case applications showing how industrial enterprises deploy semi-finished stock to address high abrasion, corrosive chemistry, impact shocks, and extreme bearing loads.
Our modified Nylon Ring Cushions and high-impact hammer buffers absorb kinetic impact forces during diesel and hydraulic pile driving operations. Replacing laminated phenolic or hardwood blocks, our cast blocks resist splintering and deliver a continuous working lifespan exceeding 300 driving cycles.
Handling sticky bauxite, wet coal, or abrasive ore concentrates causes costly downtime from material hang-ups and bridging. Ultra-high molecular weight polyethylene (UHMWPE) and lubricated Green MC Nylon sheets line bunker walls, drop hoppers, and railcar beds to ensure smooth, unassisted discharge.
Precision-milled POM-C and virgin HDPE sheets meet direct food contact regulatory standards. They exhibit virtually zero moisture absorption (<0.2%), preventing bacterial penetration and size growth during clean-in-place (CIP) hot sanitization washes along automated beverage bottling lines.
Subjected to salt spray, aggressive tidal currents, and intense ship hull contact friction, our UV-stabilized black and yellow HDPE/UHMWPE dock facing plates preserve steel wharf pilings without delaminating, cracking, or degrading from extended marine immersion.
Telescopic boom pads milled from molybdenum disulphide (MoS2) filled cast nylon operate with minimal stick-slip and friction coefficients down to 0.12. This prevents crane boom judder and avoids grease contamination across heavy lifting systems.
Polypropylene (PP) and Fluoropolymer (PTFE) sheets serve as the primary defensive barrier for acid pickling baths, electrochemical galvanic tanks, and semiconductor ductwork handling concentrated nitric, sulfuric, or hydrochloric acid solutions.
A strategic overview for supply chain directors and engineering procurement teams managing volatility, sustainability demands, and specification compliance.
The standard pure polymer sheet is increasingly upgraded with functional microscopic additives. We formulate internally lubricated cast nylon using liquid oil dispersed at the casting stage, ceramic micro-spheres for enhanced abrasive resistance, and carbon-fiber infusions to yield surface resistivities in the static dissipative range (10⁶ to 10⁹ Ω/sq) for explosive and cleanroom industrial environments.
International procurement groups are transitioning away from evaluating price-per-kilogram alone to measuring multi-year total operating costs. High-performance cast stock minimizes maintenance interventions, lowers power consumption by reducing parasitic mechanical drag, and extends preventative inspection intervals across complex assembly lines.
Top-tier equipment builders demand full batch transparency. Every production run from SHUNDA is paired with complete material test reports (MTR), confirming melt density, shore hardness, thermal deflection limits, and ultrasonic thickness mapping to prevent non-conforming shipments.
Expert answers provided by our materials scientists and foundry engineers addressing resin properties, machining parameters, and export procurement logistics.
Cast Nylon is created via an unpressurized chemical casting process that yields polymer chains with higher molecular weight and superior crystallinity. This gives Cast Nylon higher tensile strength, improved rigidity, higher heat deflection limits, and lower moisture absorption compared to extruded counterparts. Extruded PA6/PA66 is ideal for smaller, high-speed thin-wall production, whereas Cast Nylon excels in heavy sections and heavy mechanical load-bearing applications.
Unannealed sheets suffer from skin-to-core thermal gradients. We pass all semi-finished cast slabs through custom automated hot-oil annealing chambers where internal stresses are uniformly neutralized. For high-aspect-ratio thin parts, we recommend roughing both faces evenly before performing final finishing cuts to maintain close tolerances down to ±0.05 mm.
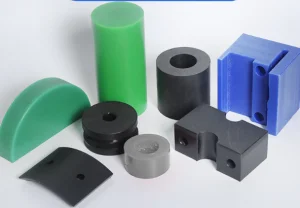
Yes. Aside from standard natural (white/ivory) and blue hues, we regularly formulate custom green lubricated PA6, graphite-filled black, flame-retardant V-0 grades, and UV-stabilized blends for outdoor installations. All chemical additives are compounded directly into the monomer melt to ensure uniform distribution through the entire thickness of the sheet.
Every commercial export consignment is backed by a complete documentation package: Certificate of Analysis (COA) / Mill Test Certificate (MTC), ISO 9001 compliance verification, RoHS/REACH compliance records where applicable, fumigation certification for wooden pallets, alongside detailed commercial invoices, packing lists, and bills of lading.
Explore our comprehensive fabrication capabilities including fluoropolymer sheets, wear-resistant liners, high-load cushion blocks, and tailored precision profiles.






Whether you require standard full-dimension semi-finished slabs (1000×2000 mm, 1220×2440 mm) or high-volume CNC finished mechanical components, our production specialists will review your blueprints and provide certified pricing within 12 hours.