
Featured Industrial Solid Rod & Stock Profiles
Explore our flagship heavy-duty PA6 extruded rods, cast monomer (MC) cylinders, and precision wear polymers exported directly to Tier-1 machinery producers and global engineering distributors.







Global Commercial Landscape: PA6 Bar Technical Demands
In modern industrial mechanical engineering, the structural displacement of ferrous alloys and brass with semi-crystalline Polyamide 6 (PA6) extruded and cast stock constitutes an essential engineering strategy for weight reduction, noise damping, and lubrication-free operation.
Controlled Annealing & Stress Relief
The prominent failure mode in heavy CNC lathe turning of raw polyamide bars is deformation caused by retained interior stresses. SHUNDA operates computerized thermal cycle annealing kilns, holding temperature plateaus that optimize crystalline morphology, eliminating center-line porosity and yielding high dimensional stability during aggressive milling.
Tribological Performance Engineering
Solid PA6 bars maintain a dynamic coefficient of friction as low as 0.15 to 0.28 against hardened ground steel surfaces. Under high loads and low-to-medium sliding velocities, PA6 bars deliver outstanding anti-galling behaviors, eliminating dry-running seizure risks in unlubricated assemblies across agricultural and harbor cranes.
Raw Material Purity & Batch Traceability
Leveraging 100% virgin caprolactam monomer and high-viscosity PA6 polymers, SHUNDA enforces strict purity controls free from unblended regrind. Every master batch undergoes Melt Flow Index (MFI) and differential scanning calorimetry (DSC) evaluation to ensure batch-to-batch consistency for critical defense and aerospace components.
Comparative Mechanical Analysis: Engineering Polymers
Evaluating engineering polymer rod candidates demands empirical material quantification. The engineering matrix below contrasts standard PA6 Bar properties against POM (Acetal), UHMWPE, and PTFE to guide procurement decisions.
| Property Metric (Standard Test) | PA6 Extruded Bar | Cast MC Nylon (PA6G) | POM-C (Polyacetal) | UHMWPE Solid Stock |
|---|---|---|---|---|
| Tensile Strength at Yield (ISO 527) | 82 – 85 MPa | 88 – 95 MPa | 67 – 70 MPa | 22 – 28 MPa |
| Modulus of Elasticity in Tension | 3,200 MPa | 3,450 MPa | 2,800 MPa | 700 – 900 MPa |
| Charpy Notched Impact Strength | 5.5 kJ/m² | 4.5 kJ/m² | 6.0 kJ/m² | No Break (>100) |
| Continuous Service Temp (Air) | -40°C to +105°C | -40°C to +120°C | -50°C to +100°C | -150°C to +80°C |
| Coefficient of Linear Thermal Expansion | 80 × 10⁻⁶ K⁻¹ | 75 × 10⁻⁶ K⁻¹ | 110 × 10⁻⁶ K⁻¹ | 150 – 200 × 10⁻⁶ K⁻¹ |
| Equilibrium Water Absorption (23°C, 50% RH) | 2.6 – 2.8% | 2.2 – 2.4% | 0.2% | < 0.01% |
Heavy Load Transmission
Compared with Acetal (POM), PA6 bar stock exhibits 20% higher impact attenuation and exceptional fatigue resistance under dynamic cyclic stress, making it the preferred raw stock for heavy spur gears, cable sheaves, and rack pinions.
Self-Lubricating Bushing Stock
Cast MC Nylon rods impregnated with internal liquid lubricants or solid MOS₂ additives drastically depress stick-slip vibration, boosting uptime in harbor crane boom slides and telescopic linkages by extending mean time between service (MTBS).
Direct Steel Replacement
At 1.14 g/cm³, PA6 bar provides a 7:1 weight advantage over tool steels and bronze, substantially reducing the rotational inertia of rotating hubs, lowering mechanical wear on gearboxes, and minimizing operational drive-energy requirements.
Localized International Compliance & Support Assurance
Global supply chain resilience depends on continuous regulatory compliance, strict packaging parameters, and clear material certification for seamless customs integration and dependable OEM application.
12-Hour SLA Engineering Desk
SHUNDA maintains a bilingual team of senior plastics engineers who provide comprehensive RFQ turnarounds, GD&T feasibility analyses, and material conversion advice within 12 hours across global time zones.
RoHS & REACH Compliance
All virgin PA6 polymers and masterbatch colorants fully comply with EU Directive 2011/65/EU (RoHS 3) and EC 1907/2006 (REACH), free from SVHC (Substances of Very High Concern), heavy metals, and prohibited plasticizers.
Precision Mill Tolerances
Bars are calibrated via centerless cylindrical grinding systems, upholding tight outer-diameter (OD) metric tolerances down to ISO h9/h10 class, preventing chuck runout and chatter during automatic bar-feeder lathe cycling.
Export Sea-Freight Crate Packaging
Polymer bars are protected against ambient moisture and UV degradation via multilayer poly-wrap, strapped within fumigated solid plywood crates and desiccant-loaded barrier bags to eliminate cross-ocean dimensional distortion.
Localized Application Scenarios & Case Realities
Across diversified international industrial clusters, PA6 bars from SHUNDA are turned into mechanical parts that operate under harsh mechanical loads, caustic chemicals, and wide temperature swings.
European Heavy Forestry & Port Cranes
Component: Wire rope guide sheaves and articulated swing-pin bushings.
Operational Challenge: Extreme impact spikes, salt spray corrosion, and continual steel wire abrasiveness.
Outcome: Switching to cast oil-filled PA6 round bar increased wire rope operational life by over 300% and lowered deadweight overhead boom mass by 65 kilograms per trolley module.
North American Mining & Bulk Handling
Component: Flanged track rollers, slurry pipe scrapers, and star wheels.
Operational Challenge: Intense slurry washouts and highly abrasive fine silica quartz dust entering bearings.
Outcome: Natural Cast PA6 bars converted on 5-axis CNC machining stations yielded components that absorb grit without seizing, operating smoothly in continuous copper mine conveyor circuits.
Southeast Asian Palm Oil Bottling Conveyors
Component: Timing screws, indexing starwheels, and high-velocity neck guides.
Operational Challenge: Caustic washdown chemicals, continuous friction, and sanitation compliance.
Outcome: Food-grade natural white PA6 bars provided high chemical resistance and exceptional impact strength, reducing line noise levels from 88 dB to under 72 dB.
Technology Roadmap & Sustainable Polymer Engineering
SHUNDA continues to invest in continuous reactive casting, smart additive compounding, and low-carbon circular polymer economies. Our engineering development roadmap highlights key advancements in modern polyamide manufacturing.
High-Purity Cast Monomer PA6 with Nano-Graphene Enhancements
Integrating exfoliation-grade graphene platelets into liquid caprolactam monomer prior to mold polymerization. This matrix architecture increases flexural modulus past 4,200 MPa while imparting electrostatic dissipation (ESD) paths (10⁶ to 10⁹ Ω/sq) for explosive and hazardous chemical extraction environments.
Continuous Ultrasonic Center-Line Porosity Detection
Deploying multi-transducer inline acoustic phased-array inspection systems across all PA6 bar casting lines above Ø 100mm. This real-time non-destructive testing (NDT) identifies micro-void shrinkage cavities in the stock core, guaranteeing zero-defect profiles for demanding machining runs.
Bio-Sourced Chemical Recycled Feedstock Streams (ISCC+ Certified)
Advancing towards net-zero carbon footprints by integrating chemically depolymerized post-industrial PA6 residues into virgin-grade caprolactam streams. This closed-loop recycling preserves 100% of prime mechanical performance parameters while meeting stringent European automotive carbon-footprint directives.
Complementary Semi-Finished Polymers & Precision Components
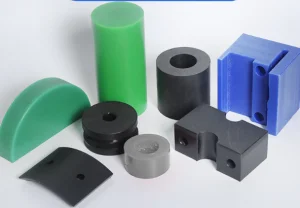
Review our extended portfolio of precision engineering stock, impact-resistant pads, hollow cast tubes, and fully customized CNC mechanical parts.







Industrial Q&A: Polyamide 6 (PA6) Bar Technical Inquiries
Comprehensive answers to frequently asked engineering and procurement questions regarding material selection, machining parameters, moisture compensation, and international shipping protocols.