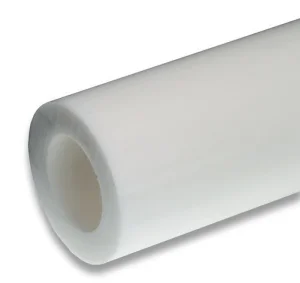
High-Performance Engineering Polyacetal & Nylon Portfolio
Direct from our Henglan Town factory base: semi-finished hollow bars, rods, and heavy machine stock for rigorous industrial duty.








Technical Superiority of POM-C (Polyoxymethylene Copolymer)
Why precision engineering departments favor POM-C hollow bars over standard homopolymers and metal alloys in hydraulic, chemical, and conveying environments.
Zero Centerline Porosity
Unlike homopolymers (POM-H) which often suffer from axial center porosity due to thermal crystallization differentials, our vacuum-assisted POM-C extrusion process guarantees a completely dense, continuous wall cross-section ideal for pressure piping.
- Eliminates internal fluid leakage paths
- Enables high-pressure dynamic sealing
- Enhances rotational balance at high RPM
Hydrolytic & Chemical Stability
Polyacetal Copolymer backbone exhibits outstanding resistance against basic solutions (alkalis), boiling water, and hydrocarbon solvents between pH 4 and 14, outperforming Nylon PA6 in wet, submerged operating zones.
- Moisture absorption lower than 0.2%
- No swelling or wall dilation in water
- Resistant to glycols, fuels, and solvents
Optimized Machining Mechanics
Extruded with multi-stage computerized thermal annealing, SHUNDA POM-C hollow stock relieves residual crystallization stresses, enabling aggressive lathe boring and external CNC milling with minimum warping.
- Chips break cleanly without gumming
- Holds sub-mil run-out across long spans
- Excellent surface finish (Ra < 0.4 μm)
Engineering Property Matrix: POM-C Pipe vs Alternative Polymers
Rigorous property testing based on ISO and ASTM standards to substantiate mechanical integrity for engineering decision-makers.
| Property Indicator | Test Standard | SHUNDA POM-C Pipe | Cast Nylon (MC PA6) | HDPE (PE100) | UHMW-PE |
|---|---|---|---|---|---|
| Density (g/cm³) | ISO 1183 | 1.41 | 1.15 | 0.96 | 0.93 |
| Tensile Strength at Yield (MPa) | ISO 527 | 68 – 72 | 75 – 85 | 24 – 28 | 22 – 25 |
| Tensile Modulus of Elasticity (MPa) | ISO 527 | 2,900 – 3,200 | 3,100 (Dry) / 1,400 (Wet) | 1,000 – 1,200 | 700 – 900 |
| Moisture Absorption Equilibrium (%) | ISO 62 (23°C, 50% RH) | 0.20% | 2.8% – 3.2% | < 0.01% | < 0.01% |
| Coefficient of Dynamic Friction (Dry) | ASTM D1894 | 0.28 – 0.32 | 0.38 – 0.42 | 0.25 – 0.30 | 0.12 – 0.18 |
| Operating Temperature Range (°C) | Continuous Service | -50 to +105 | -40 to +110 | -50 to +80 | -150 to +80 |
| Dimensional Retention in Wet State | Internal QA Protocol | Superior (Stable) | Moderate (Swelling) | High | High |
Engineered Deployment Scenarios Across Global Jurisdictions
Customized wall profiles, diameters, and mechanical chemistries formulated for complex industrial operations across North America, Europe, Southeast Asia, and the Middle East.
Food & Beverage Filling Lines
FDA-compliant white/natural POM-C tubes utilized as clean-in-place (CIP) distributor manifolds, star-wheel bushings, and bottling sleeves. Resists caustic washes and chlorine sanitizers without hydrolytic cracking.
Hydraulics & Pneumatic Guides
Heavy-wall hollow stock converted into wear sleeves, piston head back-up rings, and rod guide bearings. Resists fluid embrittlement in mineral oil, glycol fluids, and synthetic hydraulic esters.
Automotive Fuel & Emission Ducts
Precision polyacetal pipe segments installed inside diesel, biodiesel, and ethanol fuel filtration and tank sender housings. Demonstrates zero dimensional swelling under severe aromatic volatile exposure.
Electronics & Wafer Handling
Static-dissipative (ESD) modified POM-C tubes custom extruded for semiconductor wash carriers, cleanroom guide rollers, and vacuum pick-up tubes, avoiding static discharge hazards.
China Factory Supply Chain Resilience & Efficiency Advantages
Discover how SHUNDA combines raw polymer compounding, direct tubular extrusion, and downstream CNC operations to compress project schedules and trim global landed costs.
Vertical Integration from Resin to Part
By blending our own resin stabilizers and controlling continuous extrusion lines in Hebei, we supply both raw hollow stock and turn-key finished machined components, avoiding the 20-35% markup typical of trading intermediaries.
Logistical Hub & Tianjin Port Proximity
Located near the mega-port of Tianjin and modern road freight spines, SHUNDA provides regular 20ft and 40ft HQ container shipments, certified fumigated export crating, and seamless FOB/CIF/DAP terms.
Full Traceability & Material Certificates
Every batch of extruded POM-C hollow tubing is serialized with lot numbers. Customers receive raw material inspection records, tensile test reports, and RoHS/REACH compliance documentation with their order.
End-to-End Production Process & Tolerance Assurance
A structured workflow guaranteeing accurate dimensions, consistent material properties, and defect-free finishes on every production run.
Resin Desiccation
100% virgin POM-C resin is dried in dehumidified hot-air hoppers to reduce moisture content below 0.05%, preventing hydrolytic chain degradation.
Hollow Extrusion
Extrusion through oil-tempered calibrated tooling with internal mandrels guarantees consistent inner and outer wall concentricity without void defects.
Controlled Annealing
Multi-hour thermal annealing cycles in temperature-regulated oil ovens relax residual crystallization strain, preventing machining warp.
CNC Machining
High-precision turning, boring, facing, threading, and slotting to custom drawing specifications with micro-meter accuracy.
CMM QA & Packaging
Dimensional sign-off via coordinate measuring machines, non-destructive density checks, and vacuum-sealed protective maritime packing.
Technology Roadmap: The Next Generation of POM-C Pipe Solutions
Expanding the operational limits of polyacetal shapes to meet higher demands for extreme temperatures, self-lubrication, and environmental circularity.
Nano-Carbon ESD & ATEX Grades
Compounding multi-wall carbon nanotubes (MWCNTs) directly into the copolymer matrix creates a conductive pathway (surface resistivity 104 to 107 Ω/sq) without compromising structural tensile yield, designed for petrochemical and mining applications.
Solid Lubricant Infusion (POM-C + PTFE)
Internal blending of micronized PTFE and synthetic siloxane waxes lowers dry dynamic friction to 0.14, eliminating stick-slip behavior in unlubricated conveyor sleeves and dry-running food processing bushings.
Circular Bio-Attributed Acetal Pipes
Partnering with global chemical refiners to develop bio-methanol-based polyacetals with an audited ISCC PLUS mass-balance chain of custody, reducing the product cradle-to-gate carbon footprint by up to 45%.
Frequently Asked Questions on POM C Pipes & Manufacturing
Key technical and procurement answers addressing structural properties, manufacturing limits, chemical suitability, and import operations.
What is the fundamental difference between POM-C and POM-H hollow pipes? +
Can SHUNDA manufacture custom wall thicknesses and outside diameters? +
How does POM-C compare to Nylon PA6 in terms of moisture absorption and dimensional stability? +
What certifications accompany export shipments of SHUNDA POM-C tubing? +
What are your minimum order quantities (MOQ) and sample lead times? +
Precision Extruded Tubes, Engineered Plates & Heavy Profiles
Explore additional semi-finished polymers and customized machined hollow stock manufactured at our Hebei industrial production campus.