
Featured Industrial Stock & Machined Bushing Components
Standard extruded and cast polymer components engineered for tight dimensional tolerances, vibration reduction, and friction mitigation across mechanical setups.






Material Evolution: Why Polyamide Spacers Replace Brass & Aluminum
In modern electrical engineering, automotive manufacturing, and chemical processing, designers face stringent demands for reduced weight, anti-corrosion, dielectric insulation, and acoustic absorption. Nylon spacers, fabricated predominantly from Polyamide 6 (PA6), Polyamide 66 (PA66), or Monomer Casting (MC) Nylon, present structural qualities that metallic equivalents cannot match at equivalent price profiles.
High Dielectric Strength
Nylon components feature high volume resistivity and dielectric barrier capacities, mitigating electrical leakage and eliminating galvanic corrosion between disparate metallic fasteners in electronics assemblies.
Mechanical Damping & Creep Resistance
The semi-crystalline macromolecular structure of PA6/PA66 dampens high-frequency mechanical vibration, preventing nut loosening and structural fatigue in high-vibration automotive or pump assemblies.
Self-Lubrication & Chemical Inertness
Exhibiting low sliding friction coefficients (μ ≤ 0.25) against steel, nylon prevents seizing and displays sustained resistance to hydrocarbon solvents, greases, synthetic fuels, and cleaning alkalis.
Chinese Factory 4.0: Supply Chain Agility, Reshoring & Cost Compression
Finding truly cost-effective, high-yield cheap nylon spacer factories is not a race to cut resin quality. Instead, modern Hebei-based production relies on raw extrusion economies of scale, closed-loop thermal recovery, automated multi-axis Swiss CNC lathing, and unified chemical synthesis.
| Evaluation Parameter | Legacy Machining Workshops | Western Direct Distributors | China 4.0 Smart Factory (Shunda) |
|---|---|---|---|
| Feedstock Origin | Recycled post-industrial scrap mix | Virgin polymers (high markup) | Certified 100% Virgin Resins (Volume Synthesis) |
| Tooling & Setup Speed | Manual lathe setup (2-3 weeks) | Contracted third-party shops | Dual-spindle live-tooled CNC turning (≤48 hrs) |
| Tensile Strength (PA66) | 45 - 55 MPa (Air voids present) | 75 - 85 MPa | ≥82 MPa (Degassed vertical casting/extrusion) |
| Batch Cost Efficiency | Moderate (High scrap rates) | High Overhead (4x-6x Factory Cost) | Direct Manufacturer Bottom-Line Pricing |
Thermal De-Stressing
Annealing nylon spacers in regulated heating baths stabilizes internal stresses, completely eliminating post-machining shrinkage and out-of-round warping during service life.
Precision Swiss Machining
High-volume spacer turning leverages sliding-headstock automatic Swiss lathing, allowing fast throughput while maintaining unthreaded bores down to ±0.02 mm.
Material Modification
Reinforce your designs with MOS2 self-lubricating particles, 30% glass fibers (PA66-GF30) for thermal rigidity, or anti-static additives tailored to electrical equipment.
Localized Application Scenarios: Where High-Yield Spacers Excel
Nylon bushings, metric unthreaded spacers, and custom retaining rings form foundational, unheralded components across diverse global high-reliability systems.
PCB Standoffs & Telecomm Racks
Prevent short circuits between motherboard traces and metal chassis frames. Nylon spacers provide reliable standoff clearance, zero capacitive coupling, and low moisture tracking.
Automotive Engine Compartments
Used to isolate fuel delivery brackets, sensor manifolds, and wiring bundles from thermal conduction, engine block vibration harmonics, and splash corrosion.
Heavy Conveyance & Mining Assemblies
Cast MC nylon wear rings, cushion washers, and heavy spacers resist shock loads in piling machine hammer rings, crushers, and abrasive bulk-handling transfer chutes.
Industrial Polymers, Heavy Cushion Rings & Stock Bars
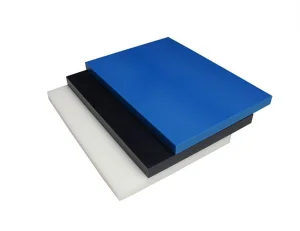
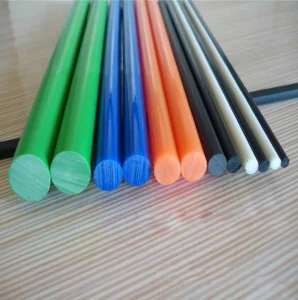
Fully certified raw extruded rounds, plate stocks, and machined wear accessories direct from our Xingtai facilities.







Frequently Asked Questions: Sourcing Nylon Spacers & Hardware
Actionable answers to help engineering, procurement, and supply-chain professionals evaluate materials, tooling, and shipping specs.
What makes sourcing nylon spacers directly from Chinese factories cost-effective without sacrificing quality?
Cost advantage is achieved through regional monomer synthesis, large-scale continuous profile extrusion, and high-speed Swiss-type multi-axis CNC machines running 24/7. When raw material supply, compounding, extrusion, and machining operate under one roof (as done by Shunda), handling costs and distributor margins are stripped out while certified virgin resins maintain physical performance.
How does nylon's moisture absorption affect spacer tolerances in damp environments?
Polyamide materials like PA6 absorb atmospheric water up to equilibrium (~2.5% to 3.0%), which causes minor volumetric swelling and increases impact toughness. For high-humidity or submerged settings requiring rigid dimensional stability (±0.01 mm), engineers should specify POM (Polyoxymethylene/Acetal), PA12, or glass-filled nylon composites (PA66-GF30) to control moisture uptake.
Can your factory machine custom spacers directly from customer CAD drawings (STEP, DWG, DXF)?
Yes. Our precision workshop handles customer 2D and 3D files (STEP, IGES, DWG, DXF, and PDF). Our engineers perform Design for Manufacturability (DFM) reviews to verify inner bore clearances, chamfer angles, and thermal tolerance budgets before starting automated production runs.
What is the difference between extruded nylon spacers and injection-molded nylon spacers?
Injection-molded spacers are cost-effective for runs of 100,000+ pieces of standard sizes, but tooling requires weeks and risks sink marks on thick-walled components. CNC-machined spacers cut from extruded or cast tube stock require zero mold tooling investment, handle thick cross-sections without voiding, and support rapid custom size adjustments.
How does Shunda ensure batch consistency and dimensional verification across large export shipments?
Every manufacturing lot follows an ISO-compliant inspection cycle: raw resin melt-flow indexing, ultrasonic internal void inspection of cast rounds, optical comparator verification, and go/no-go plug gauge inspections for through-hole diameters before export packing.