
Featured Polymer Stock & Semi-Finished Panels
Review our top-tier nylon panels, cast blanks, and engineered thermoplastic components tailored for low-friction mechanical tooling and high-abrasion wear liners.








The Real Economics of "Cheap" Nylon Panels: Total Cost of Ownership (TCO)
Why initial material cost per kilogram is an incomplete metric, and how high-integrity casting eliminates downstream machining distortion and field failures.
Optimized Resin Yield & Direct Sourcing
By producing our own virgin Caprolactam blends directly in Xinhe County, Hebei, our production ecosystem cuts intermediate broker margins by up to 28%. This ensures competitive per-ton pricing without sacrificing molecular weight or dynamic flexural modulus.
- Zero unauthorized calcium carbonate fillers
- Virgin Polyamide 6 (PA6) base monomer synthesis
- Direct batch-traceable resin chemistry
Annealing Cycles & Zero Machining Distortion
Unannealed budget nylon panels warp violently upon CNC milling due to unrelaxed thermal stresses. Every SHUNDA nylon plate undergoes computer-controlled thermal fluid annealing for up to 48 hours, eliminating internal residual tension.
- Flatness tolerance maintained below ±0.2mm/m
- High chip clearance and clean surface micro-finishes
- Negligible end-mill tool deflection during deep pocketing
Superior Wear Life Over Bronze and Steel
Replacing traditional metallic components like bronze wear plates, phosphor bush segments, or cast-iron guides with cast MC nylon panels delivers a 1:7 weight reduction, reduced kinetic power draw, and self-lubricating dry-running capabilities.
- Dynamic friction coefficient: 0.15–0.25 (dry against steel)
- Dramatically reduced counter-surface abrasion
- Shock dampening rating up to 5x higher than steel
Global Industry Development Trends in Nylon Panels
From raw monomer chemistry to nano-additive self-lubrication, the polyamide sheet market is undergoing rapid technological advancements driven by energy efficiency and lightweighting initiatives.
1. Monomer Casting (MC) Scale Supremacy
Traditional extrusion processes struggle with thick-section panels above 50mm due to inner voids and high cooling stress. The industry trend heavily favors Activated Anionic Polymerization of Caprolactam (Cast Nylon), allowing void-free slab production up to 200mm thickness with higher crystalline order and hardness (Rockwell M85–M90).
2. Nano-Dispersed Solid Lubrication
Environmental standards increasingly prohibit grease and oil lubrication in open industrial mechanisms. The adoption of MoS2 (Molybdenum Disulfide), specialized liquid graphite, and internal fluoropolymer compounding gives nylon panels self-lubricating run times over 10,000 continuous hours without maintenance.
3. Decarbonization via Metal Replacement
Automotive automated handling lines, shipyard gantry cranes, and agricultural combines are aggressively substituting fabricated metal with nylon plate structures. Every ton of nylon panel installed removes 6.5 tons of moving inertia compared to alloy steel, drastically lowering motor electricity demands.
| Polymer Variant | Specific Gravity | Tensile Strength (MPa) | Impact Strength (kJ/m²) | Continuous Max Temp (°C) | Primary Industrial Use Case |
|---|---|---|---|---|---|
| Natural MC Nylon (PA6 Cast) | 1.15 | 80–88 | > 5.0 (Charpy Unnotched) | 105°C | Wear shoes, guide plates, heavy crane outriggers |
| MC Blue Cast Nylon | 1.15 | 82–90 | > 6.0 (Charpy Unnotched) | 110°C | Large diameter gear blanks, structural drive panels |
| MoS2-Filled Black Nylon (PA6+MoS2) | 1.16 | 85–92 | > 4.0 (Charpy Unnotched) | 115°C | High-pressure slide bearings, open outdoor rails |
| Extruded PA66 Sheet | 1.14 | 75–82 | > 4.5 (Charpy Unnotched) | 95°C | Electronic precision spacers, thin punch gaskets |
| POM-C (Polyacetal Baseline) | 1.41 | 65–72 | > 6.0 (Charpy Unnotched) | 90°C | Dimensional micro-valves, wet environment bushings |
Global Enterprise Procurement Requirements & Supply-Chain Risk Mitigation
Strategic considerations for international procurement officers buying volume nylon sheets and custom components from Chinese production bases.
Moisture Absorption Control & Tolerancing
Polyamides naturally absorb ambient moisture (up to 3.0% under ISO 62 equilibration). Professional buyers must require that drawings indicate whether dimensions apply to as-molded/as-machined dry states or conditioned equilibria. SHUNDA provides sealed barrier foil wrapping for overseas containers to ensure dimensional stability upon arrival.
Consolidated Container Loading (LCL & FCL)
Buying cheap nylon panels alone can yield sub-optimal container cubic filling. SHUNDA offers integrated shipment consolidation across our complete engineering plastic lines: pairing dense nylon plates with low-density HDPE sheets, lightweight POM rods, or hollow MC nylon tubes, cutting freight cost per metric ton by up to 35%.
Verification Against Regrind Blending
Cheap nylon panels often use reground post-industrial trim, causing random brittleness and micro-crack failures under impact hammer shocks. SHUNDA includes Material Inspection Certificates (EN 10204 type 3.1) and ultrasonic density testing charts verifying total homogeneity across all sheet center-cores.
Procurement Quality Checklist for Overseas Buyers
Always specify your target: 1. Plate Flatness Requirements (DIN ISO 2768-m); 2. Planar Stress Annealing Protocol; 3. Color Uniformity Standards (Natural Ivory, Engineering Blue, Graphite Black); and 4. Packaging Barrier Safeguards against Ocean Fog Oxidation.
Macro Industry Solutions: Engineering Polyamide at Scale
Field-proven mechanical systems powered by precision-machined PA6 and MC cast nylon slab stock.
Heavy Construction & Mobile Cranes
Modern mobile telescoping boom cranes utilize cast nylon boom slider pads and outrigger stabilizer footings instead of heavy steel alloys. MC nylon panels yield predictable frictional glide, eliminate stick-slip vibrations, and prevent costly greasing maintenance that traps abrasive desert sands.
Piling Machinery & Hammer Impact Cushions
Our heavy-section cast nylon boards are customized into impact cushions for piling machines. Capable of withstanding repetitive hydraulic drop hammer impacts exceeding 500 kN, our specially annealed polyamides absorb extreme shock loads without shattering, safeguarding hydraulic heads.
Material Handling & Conveyor Systems
Beverage bottling lines, automated distribution centers, and parcel sorting hubs operate 24/7. Machined wear tracks, low-noise chain guide rails, and quiet star-wheels made from SHUNDA natural nylon panels dampen decibel levels by up to 14 dB compared to stainless steel components.
Localized Support, Regulatory Compliance & Factory Warranties
Eliminating international procurement risk through strict European and North American test certifications and dedicated engineering communication.
12-Hour Engineering Response Window
Our sales and technical support departments operate with bilingual engineering specialists. Drawings submitted in DXF, DWG, STEP, or PDF format are reviewed within 12 hours for machineability, thermal expansion tolerances, and optimal stock yield to eliminate unneeded scrap costs.
RoHS, REACH & Heavy-Metal Screening
Every commercial polymer grade dispatched is tested under RoHS Directive 2011/65/EU and REACH (EC 1907/2006). We ensure full compliance for buyers serving sensitive markets such as electrical appliance housings, clean-tech components, and food transport infrastructure.
Export Fumigation-Free Solid Palletization
Heavy nylon sheets are packed with multi-layer waterproof stretch film, corner edge protectors, and solid non-wood composite export pallets. This ensures customs clearance without fumigation holdups across North American, European, and Australian ports.
Technical Roadmap: Next-Generation Nylon Panels (2025–2030)
Where high-performance polymer science is heading and how SHUNDA is developing sustainable, highly specialized engineering panels.
Bio-Based Long-Chain Polyamides (PA56 & PA410)
To reduce petroleum dependency, our technical laboratories are validating bio-derived pentamethylene diamine polymers. These advanced formulations deliver lower moisture absorption rates (down from 3.0% to 1.4%) while maintaining high glass transition temperatures and dynamic fatigue limits.
Conductive & Anti-Static (ESD) Nylon Panels
Surface resistivity in standard polyamides exceeds 10^12 ohms/sq. For hazardous explosive grain elevators, underground mining, and precision wafer fabrication, our R&D team has engineered carbon-nanotube doped cast sheets providing permanent 10^6 to 10^9 ohms/sq static dissipation.
Closed-Loop Chemical Depolymerization
Addressing circular economy mandates, SHUNDA is piloting chemical monomer recovery units that break post-machining clean PA6 swarf back down into Caprolactam liquid, yielding 100% molecularly equivalent virgin-grade panels with a 45% reduced carbon footprint.
Frequently Asked Questions (FAQ) for Engineering Buyers
In-depth technical answers addressing material selection, tooling recommendations, and supply chain logistics.
What is the primary difference between Cast MC Nylon and Extruded PA6/66 Sheets?
Monomer Casting (MC) involves pouring liquid caprolactam into open molds, yielding high molecular weight, higher crystallinity (approx. 45–50%), superior tensile modulus, and lower internal stresses. Extruded nylon is forced through dies under high pressure, making it ideal for thin gauge panels (<10mm) but prone to residual stress in thick sections.
How do you maintain tight tolerances on machined nylon parts given moisture expansion?
We recommend machining parts slightly undersized or accounting for equilibrium swelling if used in submerged or humid conditions. Proper annealing prior to finish machining and utilizing sharp positive-rake carbide tooling with generous flood coolant prevents thermal expansion during milling.
When should an engineer specify POM (Acetal) instead of cheap Nylon panels?
Choose POM (Delrin/Acetal) when parts demand strict dimensional stability in wet environments (POM absorbs only 0.2% water vs Nylon’s 3.0%), or for precision gears with thin wall teeth. Choose Nylon for heavy shock resistance, impact hammer pads, sliding friction, and heavy load-bearing structural pads.
Can SHUNDA produce custom colors and specific slab thicknesses on demand?
Yes. Our foundry formulates natural ivory, engineering blue, molybdenum black, bright yellow, and high-visibility safety green. Standard plate thicknesses range from 5mm up to 200mm, with slab dimensions reaching 1000x2000mm and 1220x2440mm.
How does SHUNDA protect nylon sheets from warping during maritime container shipping?
Warping is typically triggered by uneven moisture absorption during long ocean transit. We stack panels uniformly on reinforced composite pallets, secure them with strapping and corner angles, and seal entire bundles inside moisture-barrier thermal plastic wraps with desiccant packs.
What is the standard production and delivery lead time for export orders?
Standard gauge stock sheets (10mm to 50mm) ship within 5 to 7 working days. Custom cast dimensions, filled polymers (MoS2, Glass Fiber), or finished CNC machined components typically require 10 to 18 working days depending on order volume and tooling requirements.
Comprehensive Engineering Plastics & Finished Components
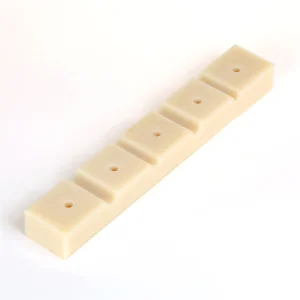
Review our secondary range of specialized wear boards, impact cushion plates, extruded bars, and engineered machining stock.





Need Precise Milling Estimates or Custom Nylon Panel Sizing?
Upload your CAD/PDF drawings or share your dimensional thickness list. Our chief polymer processing engineers will deliver complete tolerance evaluations, resin grade recommendations, and container CIF quotes within 12 hours.