
Precision Extruded UHMWPE, Polyamide & Engineering Plastic Profiles
Direct-from-factory catalog of standard round bars, extruded wear plates, and high-impact semi-finished engineering polymers engineered for severe service industrial environments.
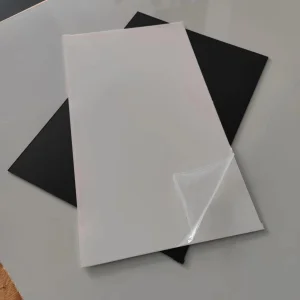
Cheap China Engineering Plastic OEM Polyamide PA6 PA66 Nylon PP UHMWPE PTFE HDPE Smooth ABS Plastic Sheet Factory Customized Color With Size For Refrigerator Door Manufacturer, Companies
View Product Specs
Discount High-Quality MC Casting Nylon PA6 HDPE UHMWPE Sheet Engineering Plastics Nylon Plastic Hard Board Sheet Supplier Exporters, Products
View Product Specs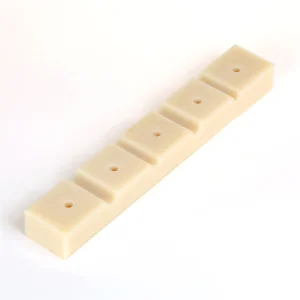
Wholesale Nylon Chain,Plastic Chain, Plastic Pad,Nylon Pad Manufacturer, Products
View Product Specs
High-Quality MC Nylon Rod Manufacturer, Exporter
View Product Specs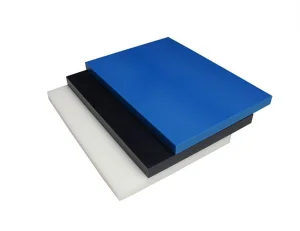
Cheap China Engineering Plastic PA6 Polyamide Nylon UHMWPE PTFE HDPE PP Plastic Sheet Board Plate Tube Rod And Bar Customized Color With Size Manufacturers, Supplier
View Product Specs
Buy MC Nylon Sheet Supplier, Company
View Product Specs
Discount Impact Blue White Black Color Nylon Ring Cushion Use For Impact Hammer For Piling Machine Suppliers, Exporters
View Product Specs
Cheap China MC Blue Cast Nylon Rod Plastic Round Rod And Bar Manufacturers, Factories
View Product SpecsMolecular Architecture of UHMWPE Solid Bar Stock
Understanding why Ultra-High Molecular Weight Polyethylene (UHMWPE / PE-1000) outperforms bronze, carbon steel, and standard polyethylenes in high-stress abrasive conditions.
Extreme Polymer Chain Entanglement
Standard High-Density Polyethylene (HDPE) possesses molecular chains containing several thousand monomer units. In contrast, virgin UHMWPE bar stock synthesizes between 100,000 to 250,000 parallel ethylene units. This enormous molecular mass minimizes chain-end density, virtually eliminating stress crack initiation under cyclical dynamic shock loads and sub-zero impacts down to -200°C.
Continuous Ram Extrusion vs. Compression Sintering
Industrial UHMWPE bars cannot be melt-processed via conventional single-screw extruders due to their extreme melt viscosity (zero melt flow index). SHUNDA employs high-tonnage multi-cavity ram extrusion systems and hydraulic compression sintering, ensuring complete particle fusion, homogeneous density distribution (0.93 - 0.945 g/cm³), and zero internal voiding for precision machining.
Thermal Annealing & Stress Relief
Uncontrolled internal stresses in polymer bars result in axial warping, out-of-round bore ovality, and dimensional drift after turning or milling. Every SHUNDA UHMWPE and MC Cast Nylon round bar undergoes a secondary computer-controlled circulating hot-air annealing cycle. This releases crystallization stresses, guaranteeing ISO 2768-m or DIN h9/h10 machining tolerances.
UHMWPE Bar vs. Alternate Engineering Polymers
A rigorous comparative analysis to assist design engineers and technical buyers in specifying the optimal polymer for wear strips, sliding guides, bushings, and chemical valves.
| Property & Test Standard | Virgin UHMWPE (PE-1000) | Ceramic-Filled UHMWPE | MC Cast Nylon (PA6C) | POM-C (Polyacetal) | PTFE (Virgin Teflon) |
|---|---|---|---|---|---|
| Molecular Weight (10⁶ g/mol) | 5.0 – 9.0 | 4.5 – 7.0 | N/A (Cross-linked) | N/A (Polyacetal) | 0.5 – 1.0 |
| Density (g/cm³, ISO 1183) | 0.93 – 0.94 | 0.98 – 1.05 | 1.15 – 1.16 | 1.41 – 1.42 | 2.15 – 2.20 |
| Yield Tensile Strength (MPa, ISO 527) | 21 – 25 | 28 – 35 | 78 – 85 | 65 – 70 | 20 – 30 |
| Charpy Notched Impact (kJ/m², ISO 11542) | ≥ 100 (No Break) | ≥ 70 | ≥ 4.5 | ≥ 6.0 | ≥ 16 |
| Sand-Slurry Relative Abrasion Index (%) | 100 (Baseline) | 55 (Superior Wear) | 180 – 220 | 200 – 250 | 350 – 400 |
| Dynamic Coeff. of Friction (Dry on Steel) | 0.10 – 0.15 | 0.12 – 0.18 | 0.35 – 0.42 | 0.25 – 0.32 | 0.04 – 0.08 |
| Water Absorption Saturation (23°C, ISO 62) | < 0.01% | < 0.01% | 6.0 – 7.0% | 0.80% | < 0.01% |
| Continuous Service Temp Range (°C) | -200 to +80 | -150 to +90 | -40 to +105 | -50 to +100 | -200 to +260 |
Global Enterprise Sourcing Demands for UHMWPE Bars
Addressing the critical risk factors, quality criteria, and total cost of ownership (TCO) benchmarks demanded by procurement managers across North America, Europe, and Asia-Pacific.
Lot-to-Lot Resin Traceability
Tier-1 equipment manufacturers reject unpredictable virgin polymer blends. Tier-1 buyers require certified melt index tests, intrinsic viscosity reports, and genuine virgin resin verification (such as Sinopec or Celanese GUR feedstock). Every master batch at SHUNDA is documented with batch numbers, retention samples, and raw material mill certificates.
Inventory Buffers & Just-In-Time (JIT) Consignment
Lead time variance disrupts automated production lines. International stockists and MRO contractors require suppliers to maintain standard stock profiles—diameters from 10mm up to 350mm—ready for immediate container loading, partnered with clear incoterms (FOB Tianjin, CIF Hamburg, DDP Long Beach).
Near-Net Shape Pre-Machining Support
Procuring raw bars often incurs massive chip waste, freight overhead, and machine spindle hours. SHUNDA bridges raw stock supply with in-house 5-axis CNC machining, centerless grinding, and profile peeling, supplying finished guide rails, bushings, and star wheels directly to OEM drawings.
Export-Grade Protective Packaging
UHMWPE's smooth, non-polar surface is prone to scraping, while long slender bars can bow under freight stacking. Strict enterprise standards dictate heavy-gauge vacuum thermal wrapping, rigid wooden cases with internal structural bulkheads, and corner protection to preserve roundness during oceanic transit.
China Direct Manufacturing: The SHUNDA Supply Chain Edge
Combining complete vertical integration, Hebei manufacturing industrial clusters, and 20+ years of dedicated polymer processing to deliver unmatched cost-to-performance ratio.
Complete Vertical Process Integration
From initial monomer blending, pigment dispersion, and ultra-high molecular polymerization handling to high-precision extrusion, stress annealing, and multi-axis CNC milling. Eliminating intermediary toll processors delivers a 22–35% direct cost advantage directly to international procurement buyers.
Advanced Custom Compounding Formulations
Need modified bars tailored to application challenges? Our in-house compounding facility produces MoS2 (molybdenum disulfide) self-lubricating bars, Boron-filled neutron shielding grades, Glass/Ceramic microsphere filled abrasion barriers, and Carbon-black conductive/anti-static (ESD) bars.
Unrivaled Capacity & Rapid Tooling
With dozens of automated extrusion lines and continuous hydraulic compression units running 24/7 in Xingtai, Hebei, SHUNDA provides rapid die fabrication for non-standard profiles within 7 business days, preventing OEM project delays.
Global Regulatory Frameworks & Certified Assurance
Stringent compliance documentation ensuring effortless import customs clearance and industrial conformity across regulated Western jurisdictions.
FDA 21 CFR 177.1520 & EU 10/2011
Certified direct-food-contact compliance for bottling, meat packing, dairy handling, and pharmaceutical conveying components. Our virgin natural UHMWPE round bars release zero migratory monomers, phthalates, or heavy metal stabilizers, meeting strict FDA extraction limits.
RoHS 3 (EU 2015/863) & REACH SVHC
Full spectrum environmental verification confirming absence of polybrominated diphenyl ethers, cadmium, hexavalent chromium, lead, mercury, and 230+ substances of very high concern. Comprehensive third-party SGS/TUV audit documentation accompany every export lot.
ISO 9001:2015 & Inspection Protocols
Dimensional conformity verified via coordinate measuring machines (CMM) and laser micrometer calipers. Testing includes Durometer Shore D hardness (ISO 868), density pycnometry (ISO 1183), and double-notched impact testing according to ISO 11542-2 standards.
High-Value Industrial Application Environments
Where UHMWPE, MC Cast Nylon, and Polyoxymethylene solid bars deliver maximum operational reliability across global heavy industry.
Bulk Materials Handling & Mining Chutes
Used extensively for conveyor skirtboard bars, idler sleeve rollers, and impact slider beds. UHMWPE's hydrophobic wax-like surface prevents sticky lignite, bauxite, and iron ore fines from bridging or packing, dramatically reducing system cleanup downtime.
Marine Port Infrastructure & Quay Fenders
Marine environments rapidly corrode steel and rot timbers. UHMWPE fender face bars and low-friction rub strips resist UV degradation, constant seawater immersion, and severe shear forces caused by berthing container vessels and oil tankers.
Automated Beverage Bottling Lines
Machined into curved chain guide profiles, high-speed star wheels, neck-handling clamps, and timing screws. Its low coefficient of dynamic friction ($\mu < 0.12$) eliminates chain squeal, minimizes conveyor drive motor amp-draw, and eliminates product marring.
Cryogenic Valve Seats & LNG Distribution
Most fluoropolymers and elastomers become glass-brittle below -50°C. Virgin UHMWPE maintains exceptional fracture toughness and ductile sealability at liquid nitrogen (-196°C) and LNG temperatures, making it the premier choice for cryogenic quarter-turn ball valve seats.
Construction Equipment Outrigger & Slide Pads
Replaces heavy bronze or lubricated steel pads in telescopic crane booms, aerial work platforms, and pile driving cushions. High load-bearing dampening cushions shock loads without spalling or requiring external grease replenishment.
Corrosive Chemical Pumps & Fluid Metering
UHMWPE provides universal chemical resistance against strong acids, oxidizing agents, and alkaline caustics at ambient temperatures, serving as machined impellers, valve plug bodies, and piston wear rings in electrochemical plants.
Emerging Technological Trends in UHMWPE Processing
How polymer nanotechnology, cross-linking innovations, and sustainable manufacturing are shaping the next decade of ultra-high molecular engineering plastics.
Cross-Linked UHMWPE (X-UHMWPE)
Using precise electron beam (e-beam) or gamma irradiation to form three-dimensional covalent links between molecular chains. This increases wear resistance by up to 40% while dramatically reducing microscopic particulate shedding in medical prosthetics and cleanroom food lines.
Graphene & Carbon Nanotube Fillers
Integrating 0.5–2% functionalized graphene nano-platelets into the PE-1000 matrix creates ultra-low percolation thresholds. This yields permanently static-dissipative (ESD) bars (surface resistivity $10^5 - 10^9\ \Omega/\text{sq}$) without compromising tensile elongation or fracture toughness.
Closed-Loop Circularity & Regrind Recovery
Advanced mechanical reclamation methods allow strict segregation of clean industrial turnings. Blending up to 30% purified reprocessed UHMWPE with ultra-virgin resins (producing high-grade Eco-UHMWPE bars) delivers substantial ESG carbon credits and lower component costs without compromising bulk sliding performance.
Machining Best Practices: From Raw Bar to Precision Component
Practical cutting parameters and tooling geometry recommended by SHUNDA’s CNC machine shop to ensure tight dimensional stability and chatter-free finishes.
| Machining Operation | Tooling Material | Rake Angle ($\gamma$) | Clearance Angle ($\alpha$) | Cutting Speed ($v_c$, m/min) | Feed Rate ($f$, mm/rev) |
|---|---|---|---|---|---|
| Turning / Lathe Turning | Polished HSS / Micrograin Carbide | 15° – 25° | 8° – 12° | 250 – 450 | 0.15 – 0.35 |
| CNC Milling / Surfacing | Single-Flute Solid Carbide Upcut | 10° – 18° | 12° – 15° | 300 – 600 | 0.20 – 0.40 |
| Drilling / Deep Hole Boring | High Helix Drills (Wide Flutes) | 5° – 10° | 12° – 18° | 50 – 120 | 0.20 – 0.30 |
| Sawing / Blank Cut-off | Carbide-Tipped Circular Blades | 5° – 10° | 10° – 15° | 1200 – 2000 | Manual / Hydraulic Pace |
Crucial Machining Note: UHMWPE has a coefficient of thermal expansion roughly ten times greater than mild steel ($150 - 200 \times 10^{-6}\ \text{K}^{-1}$) and low thermal conductivity. Always prioritize razor-sharp, polished tool edges, high chip clearance volumes, and compressed air cooling rather than oily liquid flood coolants that risk environmental contamination.
Enterprise Buyer FAQ: Procurement & Material Selection
Clear, direct answers to common technical, logistics, and quality assurance inquiries encountered by procurement managers ordering polymer profiles from China.
Request Engineering Pricing & Certified Samples
Connect directly with SHUNDA’s technical polymer production engineers for CAD profile evaluations, material compatibility verification, or volume container quotes.
Inquire Direct: [email protected]Specialized Polymer Components, Tubes & Custom Shapes
Explore our extended series of cast nylon bushes, outrigger crane footpads, round tubing, and wear parts engineered for demanding global industry operations.

Buy Plastics Polyamide Natural MC Nylon Ring Cast Nylon Tube PA6 POM Rod Round Bar Engineering Plastic Black Polyamide PA66 Nylon PP UHMWPE PTFE HDPE ABS Plastic Ring Bar Factory, Companies
View Product Specs
China China Engineering Plastic Casting Polyamide Nylon ABS PTFE HDPE UHMWPE Plastic Sheet Tube Rod And bar Customized Color With Size Suppliers, Companies
View Product Specs
Famous Nylon ABS PP PTFE Plastic Rod Tube Bar Roller Exporters, Products
View Product Specs
Discount Hot Sale for UHMWPE Heavy Duty Jacking Pads Crane Foot Support Plate Plastic Stabilizer Pad Manufacturer, Companies
View Product Specs
Wholesale Natural MC Nylon Cast Rod Supplier, Company
View Product Specs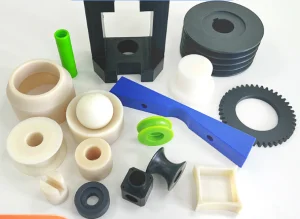
Discount MC Nylon Pad Product, Products
View Product Specs
Wholesale Engineering Plastic Polyamide PA6 PA66 Solid Nylon Rod , PTFE Rod, ABS Rod Plastic Solid Rod And Bar Customized Color With Size Factory, Companies
View Product Specs