
Featured Heavy-Duty Nylon 6 Tubes & Structural Profiles
Precision engineered hollow bars, solid stock, and mechanical components cast and extruded to extreme industrial tolerances.

China Nylon Roller Manufacturers, Company
View Specifications
Buy China Gold Supplier Nylon PA6 HDPE UHMWPE ABS PP Moulded Plastic Sheet In Large Size Companies, Products
View Specifications
OEM Plastics Polyamide Natural Mc Nylon Cast Nylon PA6 Rod Round Bar Engineering Plastic Polyamide PA6 PA66 POM Nylon PP UHMWPE PTFE HDPE ABS Plastic Rod And Bar Manufacturer, Company
View Specifications
Cheap TEFLON Rod Manufacturers, Exporter
View Specifications
Discount High-Quality MC Casting Nylon PA6 HDPE UHMWPE Sheet Engineering Plastics Nylon Plastic Hard Board Sheet Supplier Exporters, Products
View Specifications
Cheap China Engineering Plastic polyamide PA6 PA66 Nylon PP UHMWPE PTFE HDPE ABS plastic Sheet Companies, Products
View Specifications
OEM Natural Nylon Plate/Sheet, Blue Nylon Plate/Sheet Factories, Companies
View Specifications
Wholesale Engineering Plastic Polyamide PA6 PA66 Solid Nylon Rod , PTFE Rod, ABS Rod Plastic Solid Rod And Bar Customized Color With Size Factory, Companies
View SpecificationsStrategic Evolution of Polyamide 6 (Nylon 6) Tubular Engineering
How the global transition away from heavy bronze, phosphor bronze, and stainless steels is accelerating the demand for Cast and Extruded Nylon 6 hollow structures.
Total Cost of Ownership (TCO) Optimization
Modern heavy equipment manufacturers are replacing traditional bronze and steel bushings with Nylon 6 tubes. Polyamide offers an 85% mass reduction over brass, leading to lower inertia, diminished shipping logistics overheads, and dramatically lower raw stock expenditure while delivering up to 4x the operating lifespan under continuous dry friction.
Advanced Tribology & Internal Lubrication
Through proprietary monomer casting formulations, Nylon 6 tubes can be infused with liquid oil, MoS₂ (Molybdenum Disulfide), or solid waxes. These additives uniformly disperse throughout the molecular polymer matrix, effectively minimizing slip-stick, mitigating pin galling, and reducing the dependency on regular external grease applications in hazardous mining environments.
Large Diameter Monomer Casting (MC Nylon)
Extrusion tooling is naturally restricted by barrel pressures and cooling differentials, limiting heavy cross-sections. In contrast, gravity and centrifugal casting of Caprolactam monomer directly into cylindrical tooling allows the reliable manufacturing of Nylon 6 tubes exceeding 1,200mm Outer Diameter without porosity or thermal void formation.
Deciphering Global Enterprise Procurement Requirements
Procurement officers and tier-1 OEM contract manufacturers require more than basic hollow bar stock; they require batch traceability, low scrap loss, and strict stress-annealing parameters.
Coring & Machining Margin
Standard round bars waste raw material and machine hours during boring. Pre-tubed hollow stock optimizes production cycle times and cuts machine cycle scrap by upwards of 45% for sleeves, bushings, and guide rings.
Stress-Relieved Annealing
Improper cooling introduces deep residual stress in nylon walls. SHUNDA executes a multi-stage oil and air heating curve over 48 hours to ensure tubes remain completely round and straight post-turning and final boring.
EN 10204 3.1 Traceability
Industrial buyers receive genuine polymer batch certifications, including Rockwell hardness (M scale), elongation percentage, Charpy impact thresholds, and heat deflection temperatures under 1.8 MPa mechanical loads.
Moisture Conditioning Specs
PA6 naturally absorbs atmospheric moisture up to 3% at equilibrium. We consult buyers on post-machining dimensional expansion and provide vacuum-sealed or climate-stabilized shipping packaging for precise bore tolerances.
Engineering Performance Metrics: PA6 Tube vs Alternative Materials
A direct metallurgical and tribological baseline helping design engineers pinpoint when Cast Nylon 6 out-performs metals and acetals.
| Property Matrix | Cast Nylon 6 (PA6 MC) | Extruded Nylon 6 (PA6 Extrusion) | Polyacetal (POM-C) | Phosphor Bronze (CuSn8) |
|---|---|---|---|---|
| Specific Density (g/cm³) | 1.15 - 1.16 | 1.13 - 1.14 | 1.41 | 8.80 |
| Tensile Strength at Yield (MPa) | 80 - 85 | 70 - 75 | 65 - 70 | 450 |
| Compressive Modulus (MPa) | 3,200 - 3,500 | 2,800 - 3,000 | 2,800 | 110,000 |
| Coefficient of Dynamic Friction (Dry vs Steel) | 0.15 - 0.22 | 0.25 - 0.35 | 0.25 - 0.32 | 0.35 - 0.45 |
| Continuous Service Temp Range (°C) | -40 to +105 | -40 to +85 | -50 to +100 | -100 to +250 |
| Machining Tool Wear Index | Ultra Low (High Feed Rates) | Low | Low | Moderate to High |
Export-Grade Compliance & Factory Verification
Meeting international testing frameworks, regulatory directives, and robust cross-border logistical standards.
RoHS & REACH SVHC Free
All raw caprolactam monomer and plastic additives sourced at SHUNDA comply strictly with EU RoHS Directive 2011/65/EU and REACH Candidate List of Substances of Very High Concern (SVHC), protecting downstream brands against chemical non-compliance penalties.
Rapid Dispatch & Sea-Worthy Packaging
Large-diameter and thick-walled PA6 tubular products require preventative barrier packaging to eliminate ultraviolet radiation degrading and uncontrolled moisture absorption during multi-week ocean transport. Heavy palletized crates with reinforced internal banding protect dimensional integrity.
In-House CNC Secondary Machining
In addition to raw stock tubes, our Xinhe plant operates high-precision multi-axis CNC lathes and machining centers, delivering ready-to-mount sleeves, flanged bushings, crane sheaves, and cable pulleys manufactured to ISO 2768-m tolerances directly from single-source drawings.
Technological Innovations in Polyamide Extrusion & Casting
Our ongoing R&D investments targeting extreme mechanical duty, higher thermal stability, and sustainable manufacturing practices.
Nanocomposite & Ceramic Fillers
Integrating ceramic micronized particles and carbon nano-reinforcements to boost the compression yield strength of standard Cast PA6 up to 110 MPa while sustaining high elongation before break, explicitly built for deep-well marine risers.
Centrifugal Casting Automated Cells
Commissioning PLC-controlled vertical centrifugal casting cells to guarantee uniform wall thickness and concentric density in large-diameter tubular blanks, eliminating air inclusions and reducing rotational balance variation.
Closed-Loop Chemical Depolymerization
Developing in-plant recovery systems capable of breaking down clean CNC turnings back into pure monomeric caprolactam, enabling a low-carbon secondary raw stock line that matches virgin mechanical properties entirely.
Custom Finished Machining & Advanced Polymer Profiles
Explore additional engineering polymer products manufactured at our production facility in Hebei, China.

China Engineering Plastic Cast Board PA6 Polyamide Nylon ABS PP Plastic Tube Rod And Bar Customized Color With Size Factories, Products
View Specifications
Discount ODM OEM Engineering Plastic Cast PA6 Polyamide Nylon Oil Filled Nylon Rod Glass Filled Nylon Rod Plastic Tube Rod And Bar Customized Color With Size Manufacturers, Company
View Specifications
Buy Engineering Plastic Cast Board PA6 Polyamide Nylon ABS PP PTFE Plastic Rod And Bar Tube Customized Color With Size Factory, Companies
View Specifications
China Impact Round Blue Color Nylon Cushion Use For Impact Hammer For Piling Machine Supplier, Suppliers
View Specifications
China Custom CNC Machining Components Peek ABS/PTFE/Derlin/Nylon POM CNC All Kinds Of Pulley Wheel Suppliers, Exporters
View Specifications
China CNC Machined Parts Exporters, Product
View Specifications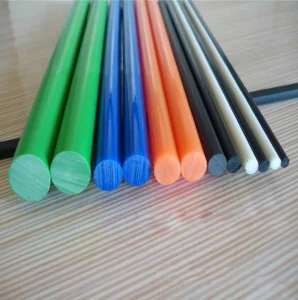
Discount Cast MC Nylon Bar Suppliers, Products
View Specifications
High-Quality China Engineering Plastic Polyamide PA6 PA66 Nylon PP UHMWPE PTFE HDPE ABS Plastic Sheet Tube Rod And Bar Customized Color With Size Suppliers, Factory
View SpecificationsProcurement & Engineering Questions Answered
Addressing the critical functional and contractual questions buyers encounter when purchasing Nylon 6 tubes from Chinese industrial plants.